2026-08-18
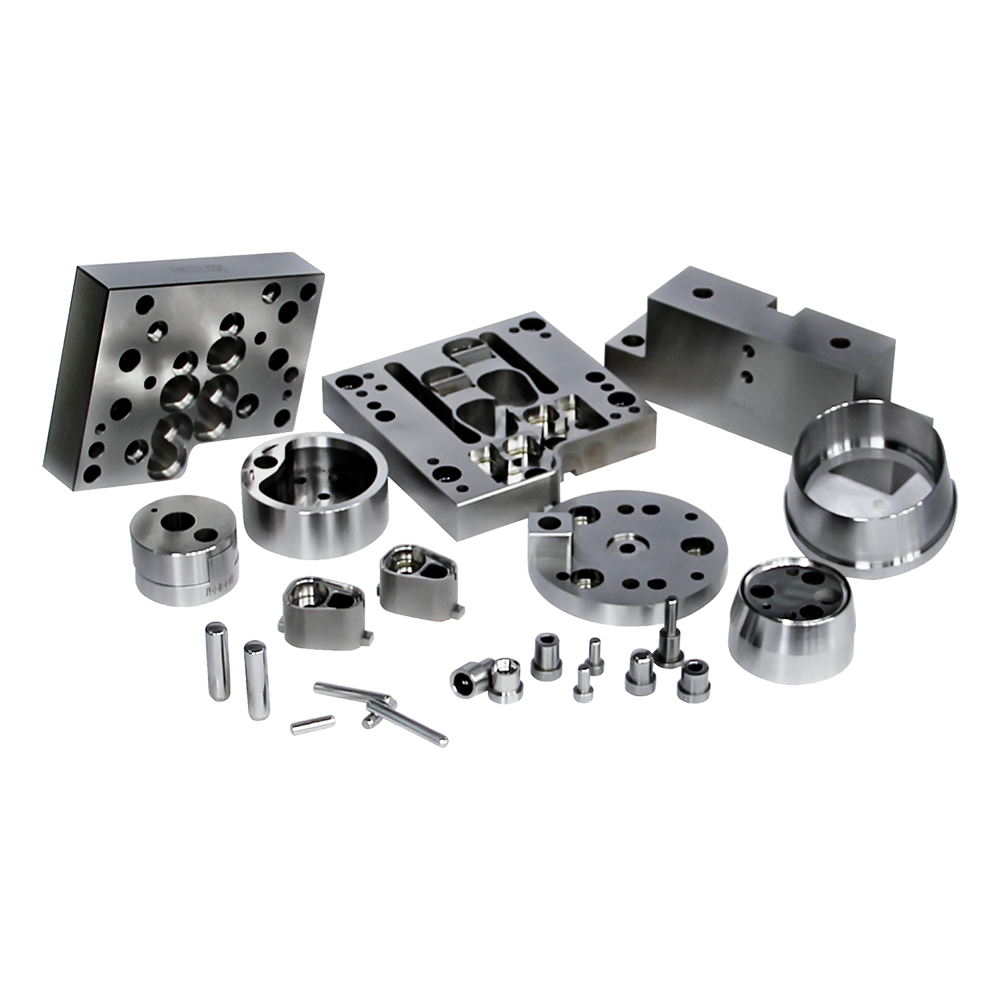
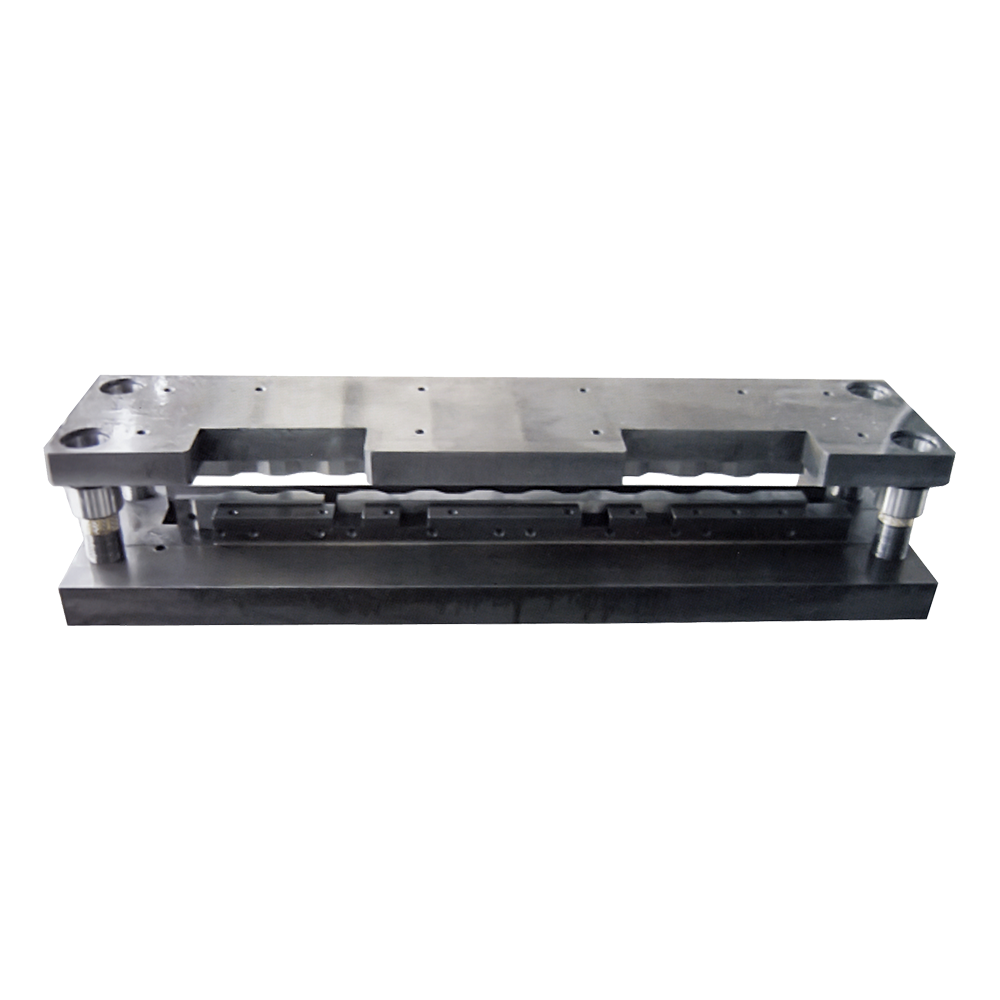
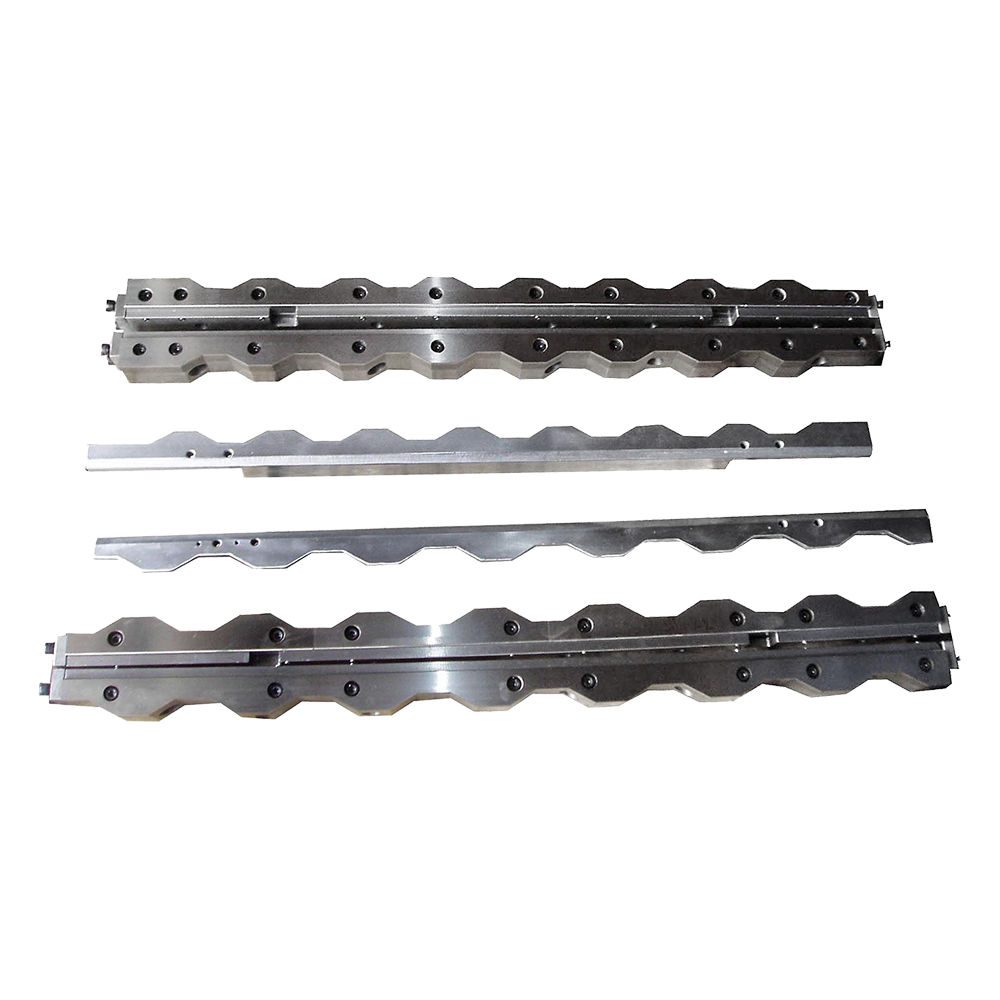
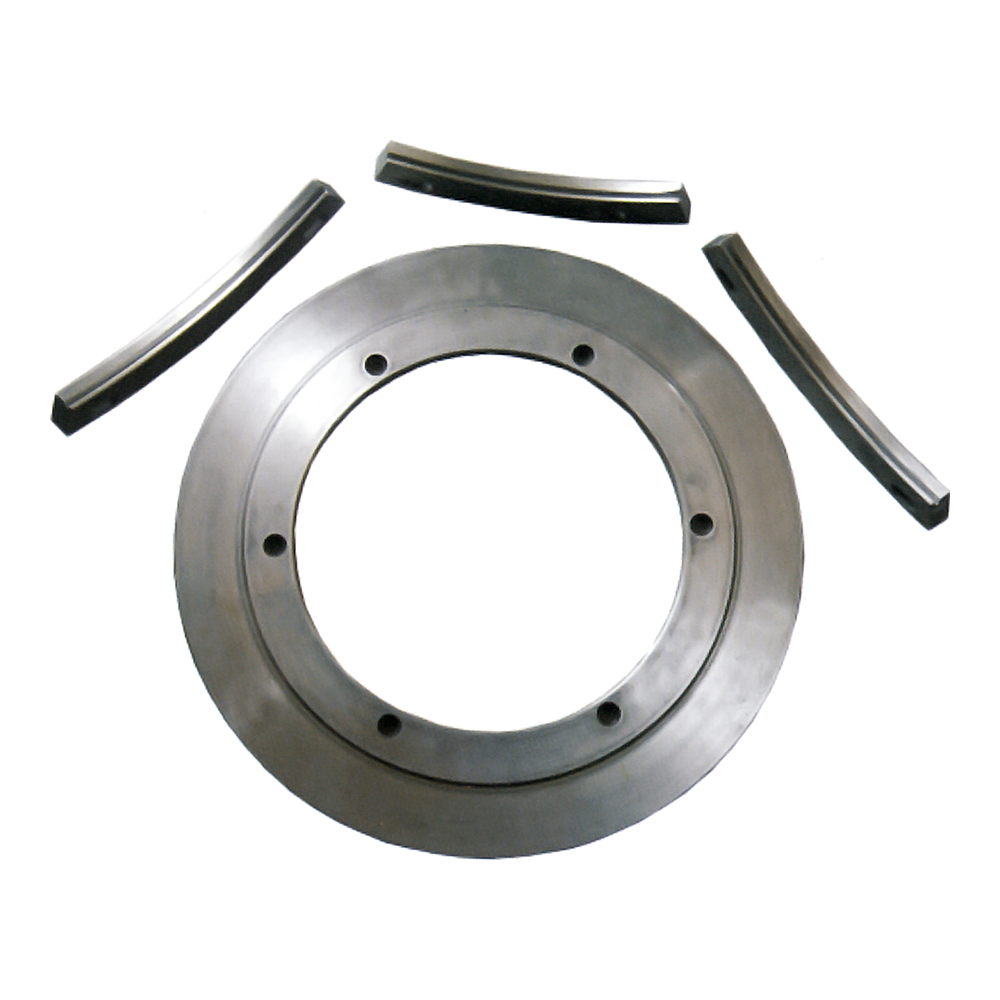
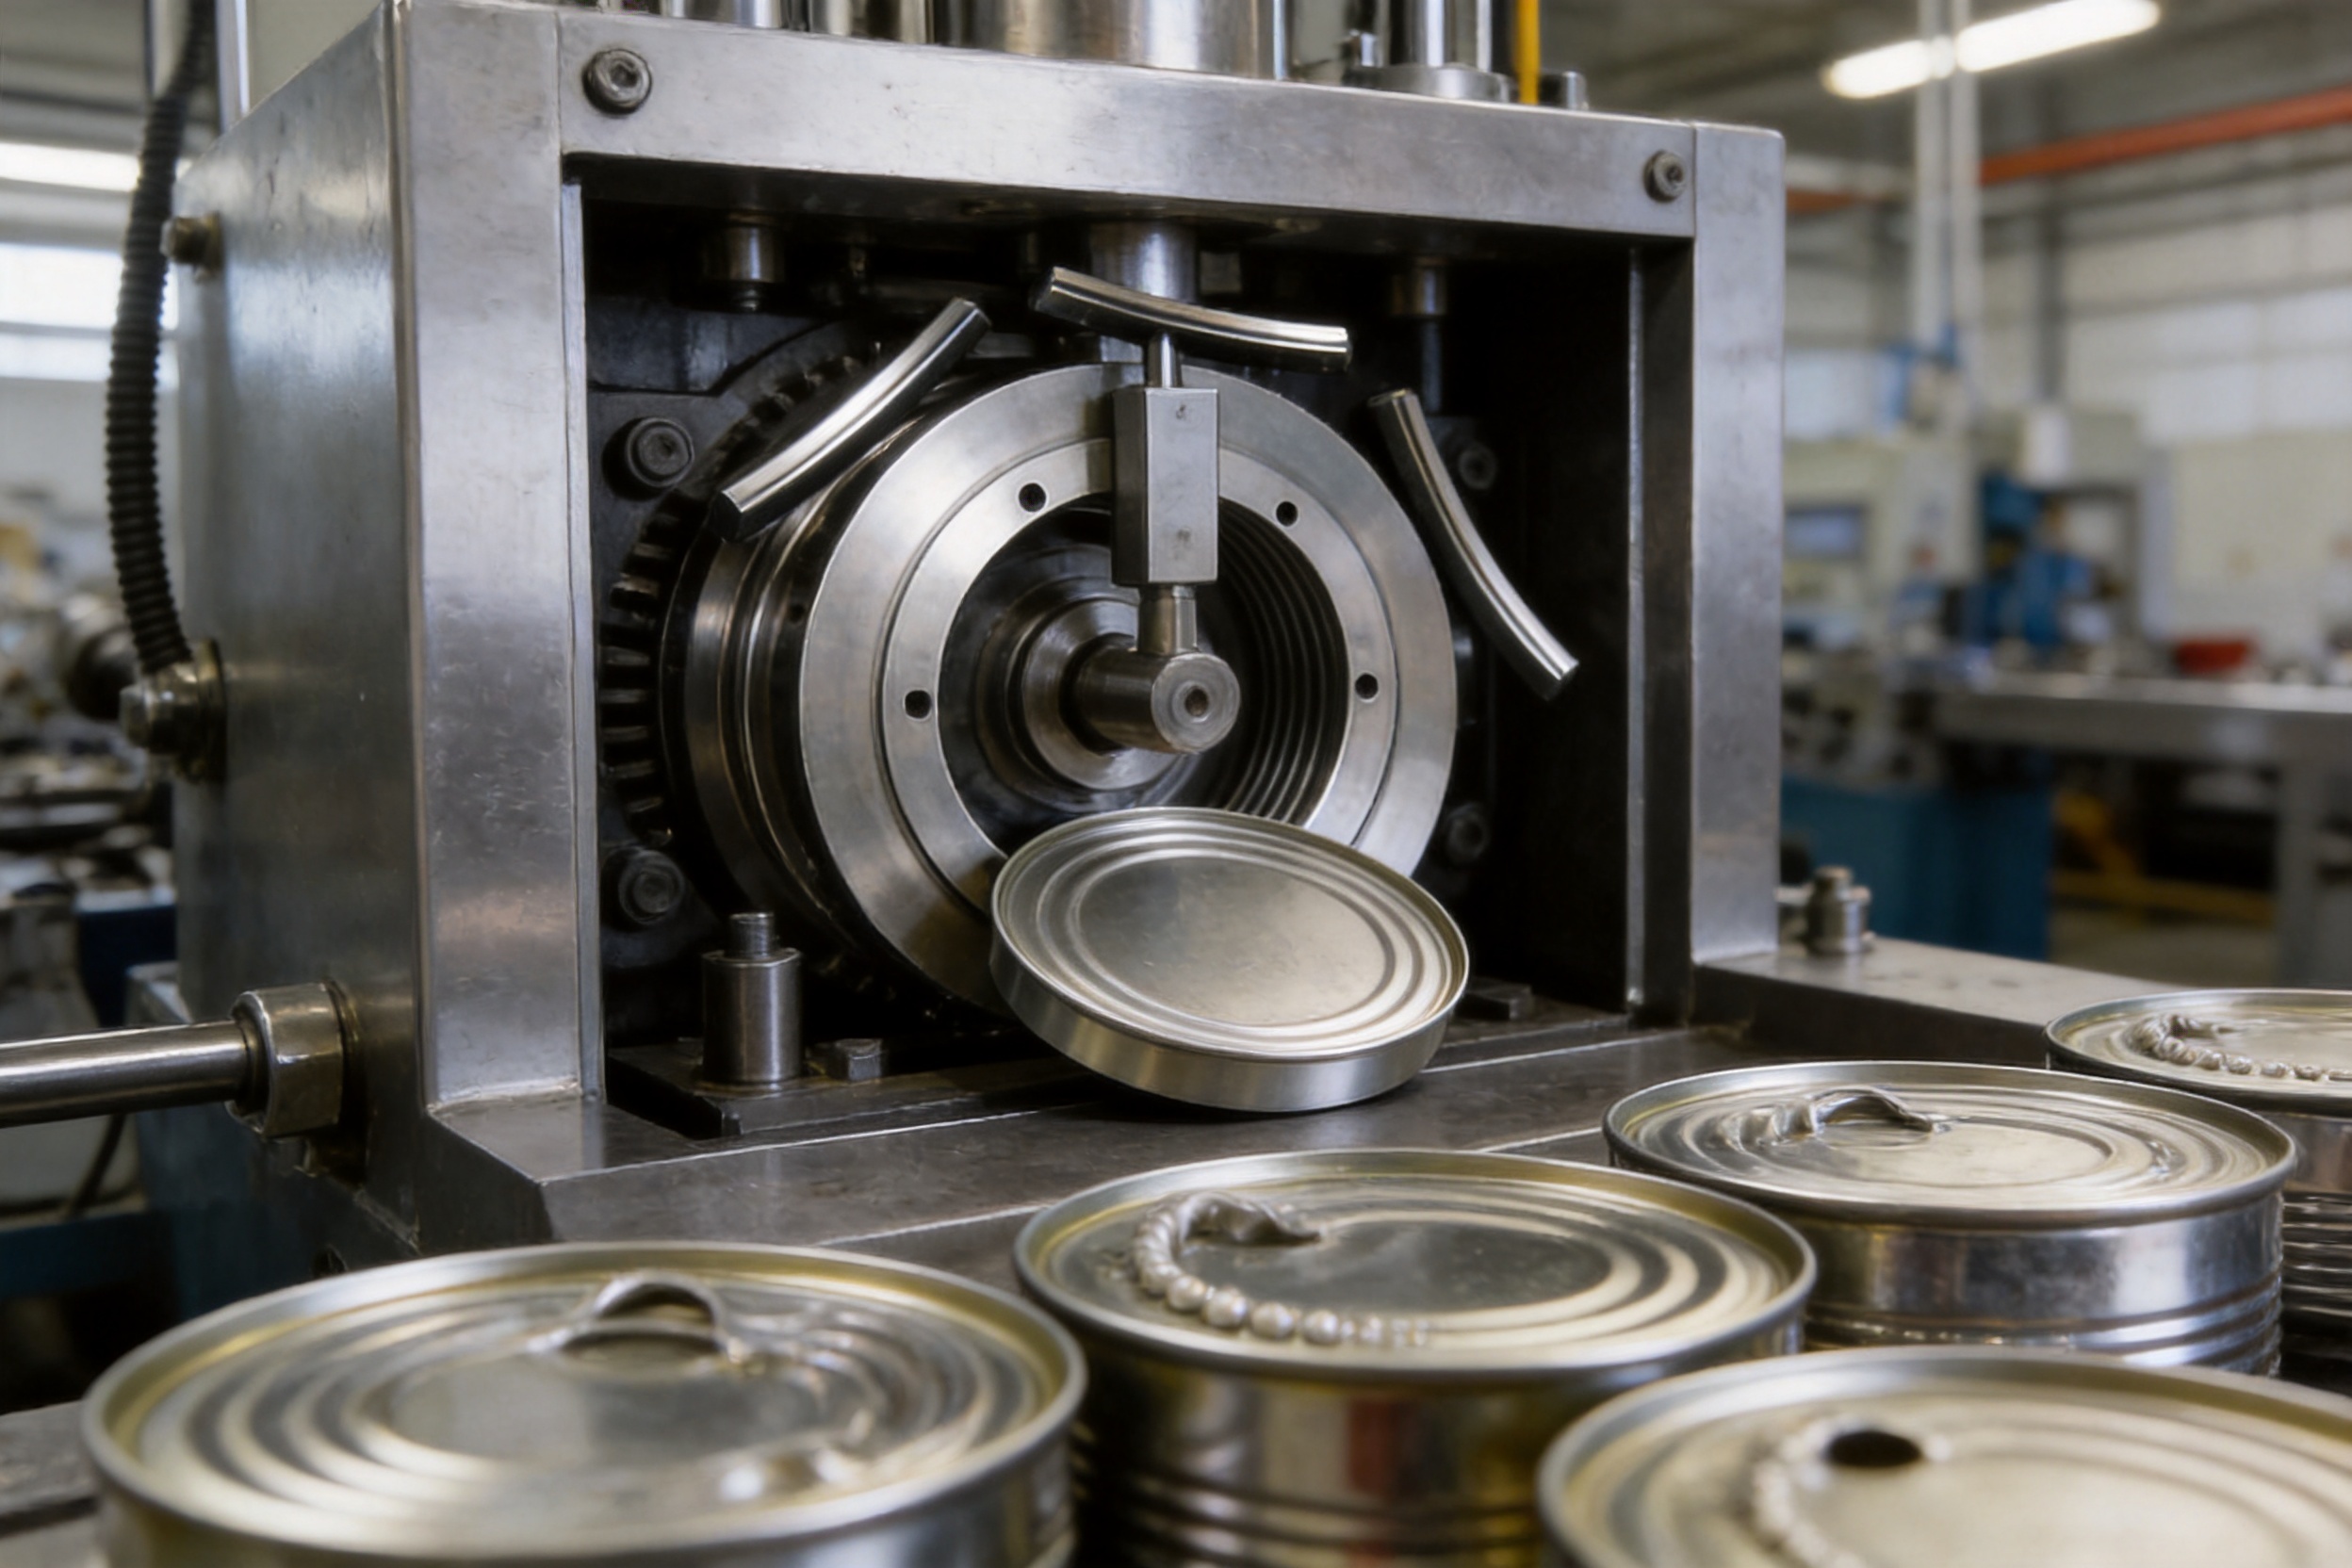
A conversion press seaming roller die is a precision mold component used in the production of metal can ends and lids. Although compact in size, the die has a direct influence on dimensional accuracy, forming stability, seam quality, production speed, and the service life of the complete conversion press. When the die is manufactured accurately and matched correctly with the press, it helps transform flat tinplate or other suitable metal blanks into consistently formed can lids with dependable profiles and repeatable performance.
For manufacturers of food cans, beverage cans, aerosol containers, chemical tanks, and other metal packaging products, the quality of the seaming roller die is an important part of the overall production system. A poorly made or incorrectly matched die may cause uneven forming, excessive wear, unstable feeding, defective curling, metal scratching, dimensional variation, and unnecessary downtime. A professionally engineered conversion press seaming roller die, by contrast, supports continuous operation and helps can makers maintain stable output over long production cycles.
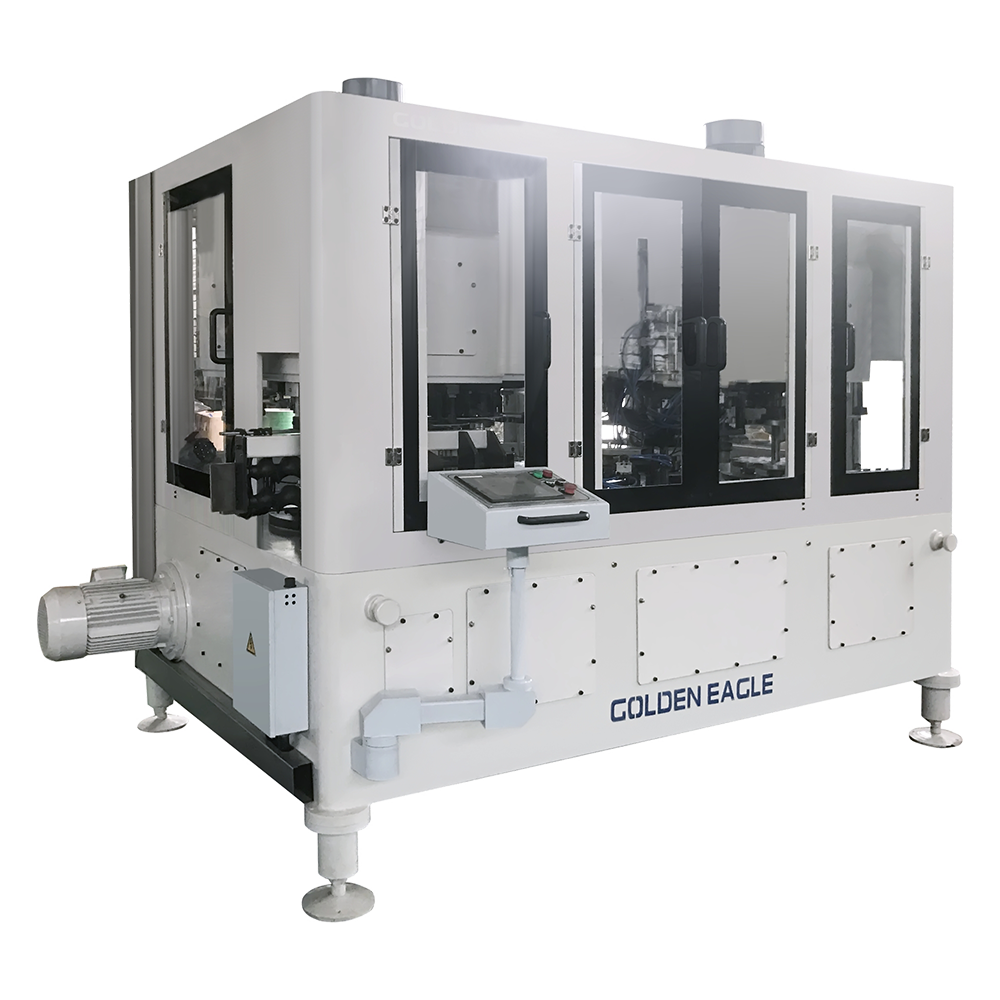
Zhejiang Golden Eagle Food Machinery Co., Ltd. produces can-making machinery and can-making molds for a wide range of metal packaging applications. With a history that began in 1978, the company has developed extensive experience in the design, machining, assembly, and application of tooling for can production. Its conversion press seaming roller die is part of a broader product range serving food can production lines, beverage can production lines, can lid production lines, aerosol canister lines, chemical tank lines, two-piece can lines, and related metal packaging systems.
Conversion Press Seaming Roller Die
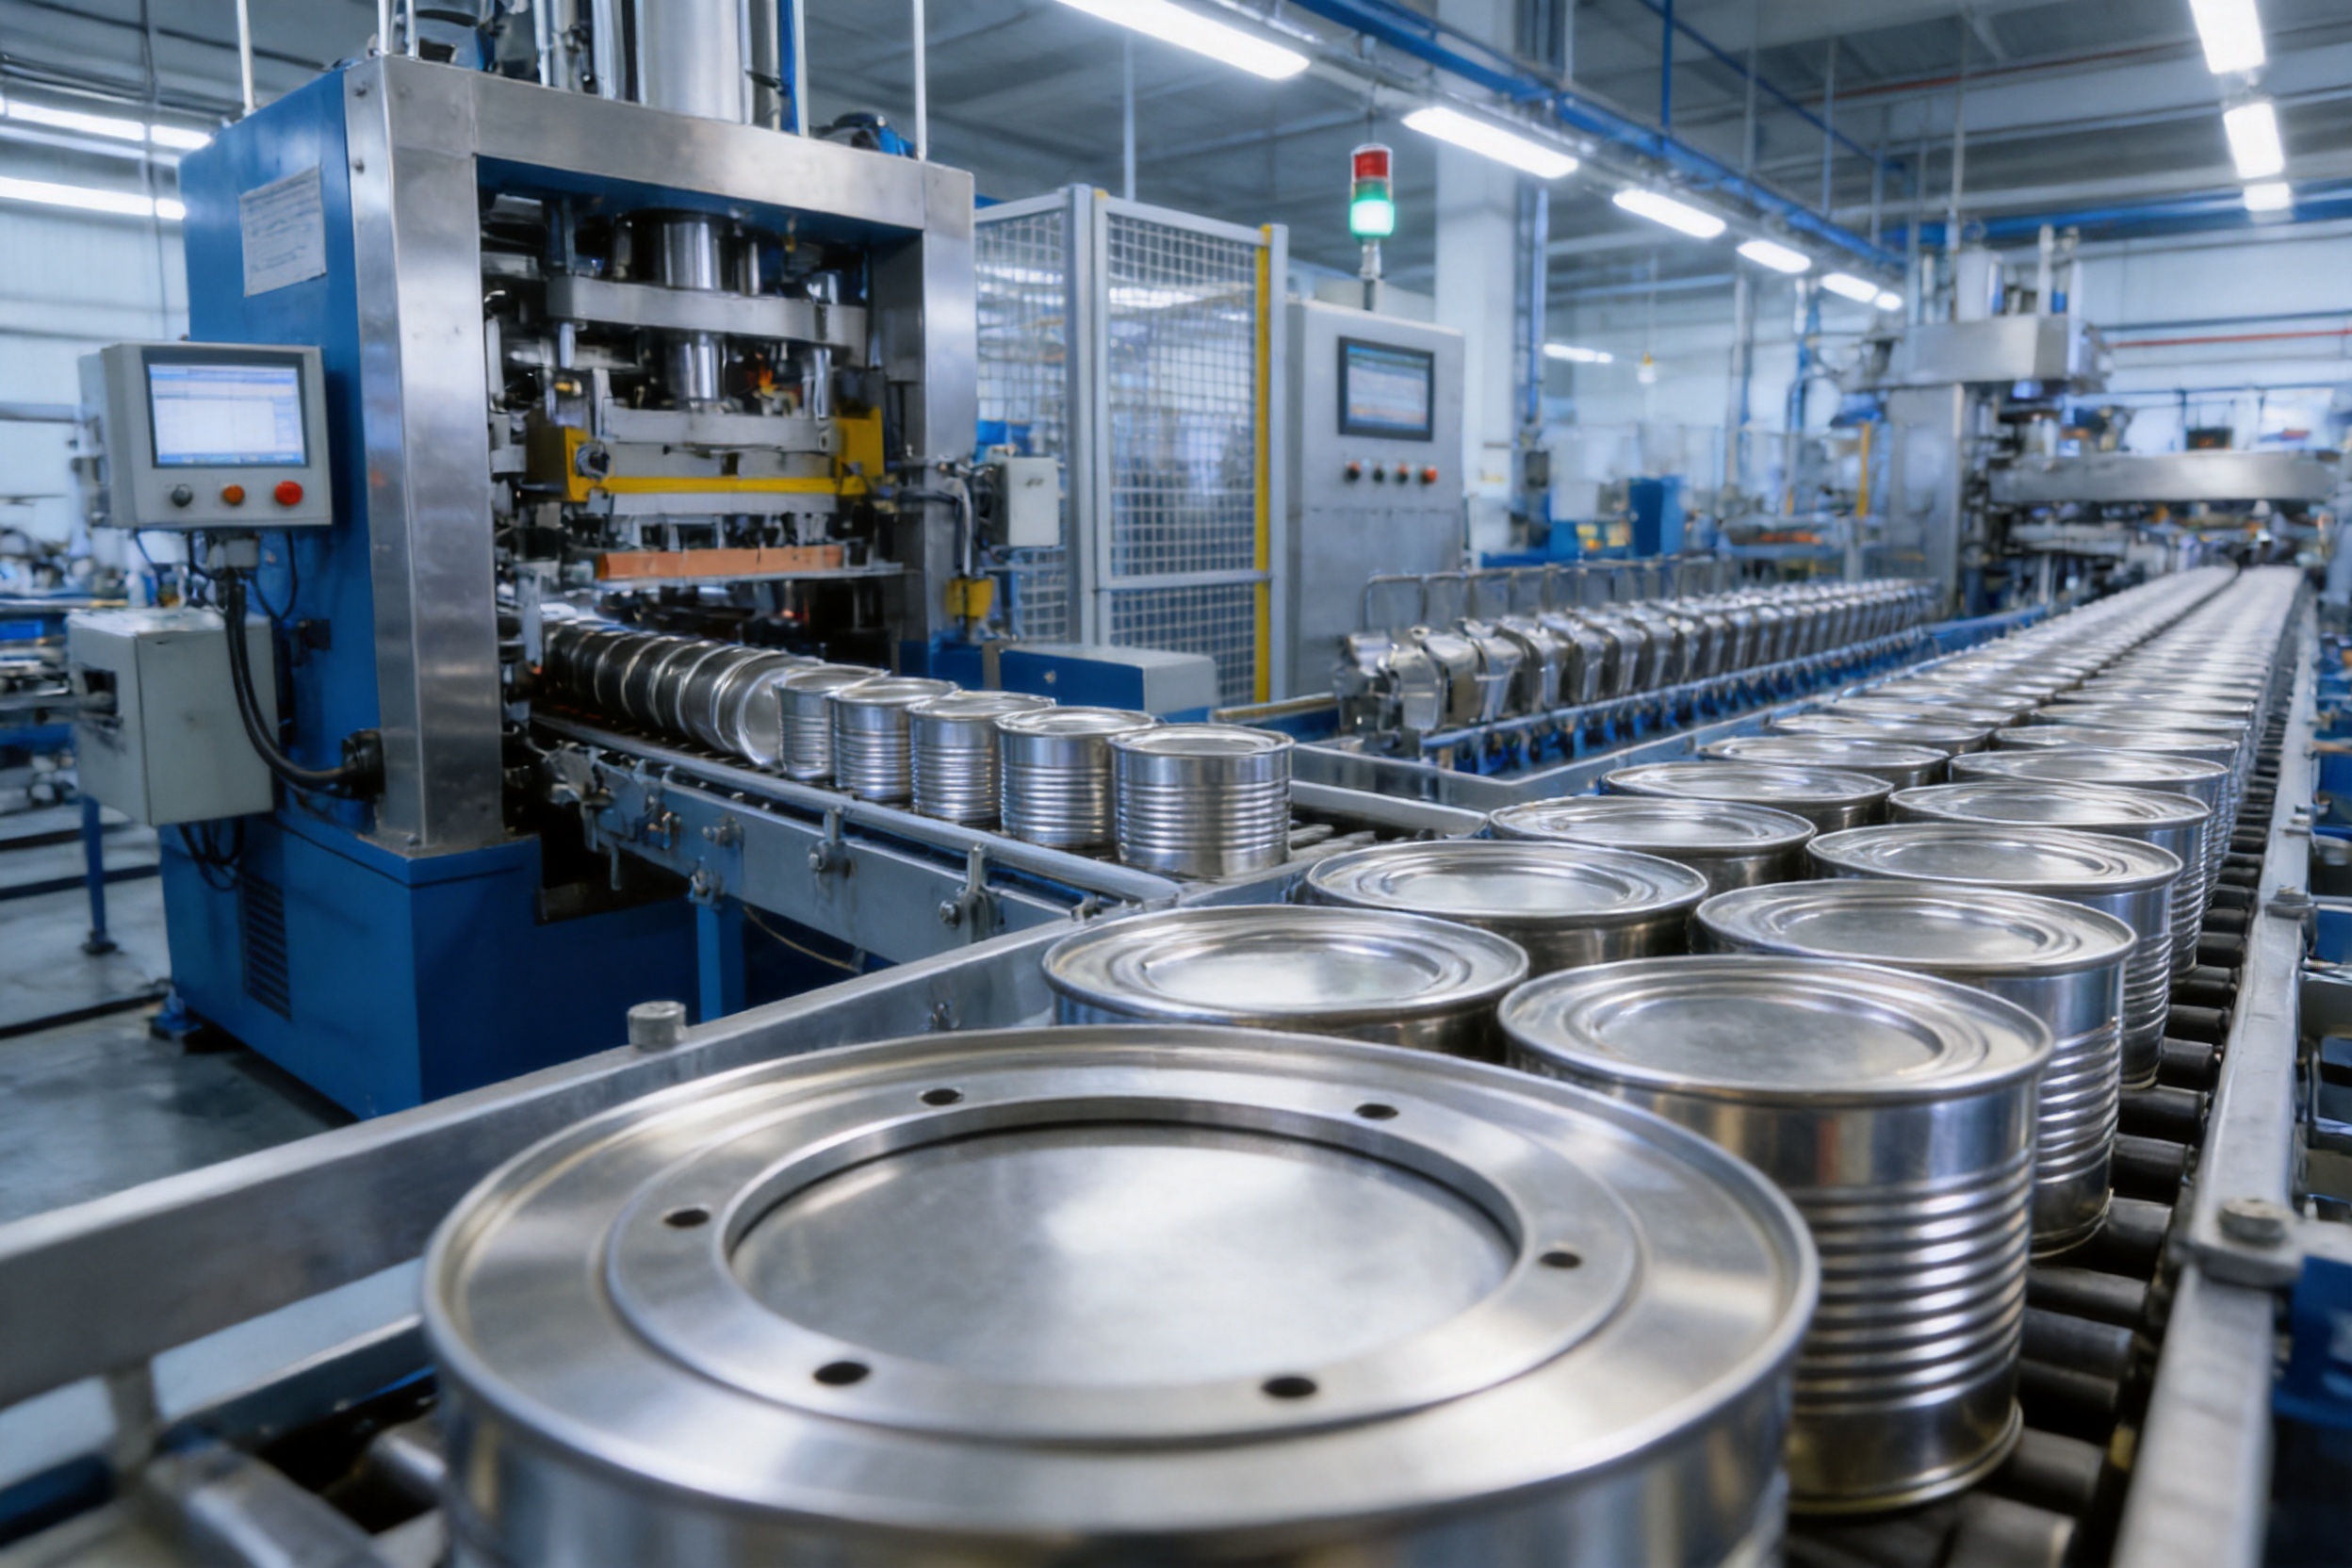
A conversion press is a machine that performs one or more forming operations on a metal blank to create a finished or semi-finished can end. Depending on the production design, the press may draw, emboss, curl, bead, score, countersink, or otherwise shape the blank. The seaming roller die is the tooling element that defines and controls a specific forming profile during the operation.
The term “seaming roller die” refers to a precision-shaped die or roller-forming component used to create the geometry required for later seaming or closure assembly. In a complete can production process, the lid must be dimensionally consistent so that it can be joined securely to the can body. The forming tool therefore has to maintain the required relationship between the lid diameter, curl, countersink, panel, bead, score area, and other functional features.
The exact configuration of a conversion press seaming roller die depends on the machine design, lid specification, metal thickness, production speed, and product application. Food cans may require a different forming profile from beverage ends, aerosol components, or chemical containers. For this reason, a standard-looking die cannot always be installed as a direct replacement without checking the original tooling data and press conditions.
A suitable die normally takes into account the following factors:
1. The outside and inside dimensions of the can lid.
2. The material type and temper of the metal sheet.
3. The material thickness and coating condition.
4. The forming sequence of the conversion press.
5. The required curl, bead, countersink, or panel profile.
6. The speed and stroke characteristics of the press.
7. The lubrication and cooling conditions used during production.
8. The required connection with downstream seaming equipment.
9. The expected production quantity and tooling service interval.
Because every conversion press and lid specification may differ, the die should be selected as an engineered component rather than as a generic replacement part.
Can lids are produced to demanding dimensional requirements. A small deviation in a critical edge or forming radius can affect how the lid is fed, stacked, sealed, and seamed. The conversion press seaming roller die plays an important role in controlling these features throughout production.
During forming, the metal blank is guided and shaped by the interaction of the press, punch, die, roller, and related tooling. The die profile determines how the material flows. If the profile is too sharp, the metal may experience unnecessary stress or surface damage. If the profile is too loose, the required shape may not be formed consistently. An accurately manufactured die provides a controlled transition between forming stages and reduces the risk of irregular deformation.
In high-volume can production, repeatability is just as important as the initial result. A die that produces one acceptable lid but gradually loses accuracy during operation cannot support efficient manufacturing. The tooling must maintain its geometry under repeated contact, pressure, vibration, and thermal changes. Its working surfaces must also be finished carefully to reduce friction and prevent damage to the tinplate coating.
The die also contributes to the production line’s overall material efficiency. Stable forming helps reduce rejected lids caused by wrinkles, splits, incomplete profiles, incorrect dimensions, or surface marks. Fewer rejected parts mean lower material consumption, less reprocessing, and better utilization of press capacity.
The primary advantage of a precision conversion press seaming roller die is its ability to produce repeatable forming results. Accurate machining ensures that the working profile follows the intended design. When the die is correctly installed and adjusted, each cycle can produce lids with closely controlled geometry.
Consistency is especially important when lids are supplied to automatic seaming machines. Automated lines depend on predictable component dimensions. If the lid profile changes from one batch to another, the seamer may require repeated adjustment, or the finished container may show an unreliable seal. A stable die helps reduce these variations at the source.
The final seam between a lid and a can body is affected by the condition of both components. The lid must arrive at the seaming operation with the correct curl and profile. An accurate roller die supports the production of a lid that can be positioned and joined more consistently.
Improved dimensional stability can help reduce common problems such as incomplete seams, loose seams, excessive overlap variation, flange damage, and irregular sealing compound compression. Actual seaming performance still depends on the complete system, including can body dimensions, lid specifications, seaming chuck condition, roll adjustment, compound application, and machine speed. However, a well-made conversion tool provides a reliable foundation for these downstream operations.
Tinplate and coated metal materials can be sensitive to scratches, dents, and coating damage. Tooling surfaces that contain machining marks, burrs, incorrect radii, or rough transitions may leave visible defects on the lid. Precision finishing helps provide a smoother contact surface and supports more controlled material movement.
Reducing surface damage is beneficial for both appearance and product protection. In food and beverage packaging, the integrity of the coating is also important because it helps protect the metal from contact with the packaged product and the surrounding environment. Tooling alone cannot guarantee coating performance, but careful tool design and finishing can reduce avoidable mechanical damage.
A die manufactured with suitable materials, accurate heat treatment where required, and controlled surface finishing can offer a longer working life than a low-quality or poorly finished alternative. Longer service life reduces the frequency of tool replacement and can help lower the cost of maintenance over the full production cycle.
Service life depends on several operating conditions, including the material being formed, press speed, lubrication, alignment, cleaning, applied pressure, and maintenance practice. A durable die is therefore most effective when it is installed and operated within the recommended conditions.
Unexpected tooling failures interrupt production and may affect the entire line. A damaged die can require inspection, removal, repair, replacement, and re-adjustment. These activities consume time and may also lead to delayed deliveries.
Accurate tooling reduces the likelihood of premature wear and unstable forming. When combined with planned inspection and replacement schedules, it helps production managers move from emergency maintenance toward controlled maintenance. This is particularly valuable for manufacturers running multiple shifts or large-volume orders.
Modern can-making plants commonly use automatic feeding systems, conversion presses, lid-making machines, inspection units, and packaging equipment in an integrated line. The tooling must work in harmony with the machine’s stroke, feeding system, guides, sensors, and downstream equipment.
A professionally supplied conversion press seaming roller die can be produced according to the relevant press model and product specification. This approach is more dependable than selecting a tool based only on general appearance or nominal size. Before manufacturing, technical data should be reviewed so that the die profile, mounting dimensions, working clearances, and production requirements are properly matched.
The performance of a conversion press seaming roller die depends heavily on the manufacturing process used to produce it. Zhejiang Golden Eagle Food Machinery Co., Ltd. has been engaged in can-making machinery and mold manufacturing for more than four decades. The company was formerly known as Zhejiang Food Machinery Factory and Zhoushan Mold Factory, reflecting its long connection with food machinery and tooling production.
The company has a workforce of more than 350 trained personnel, including experienced design and development engineers. This combination of engineering knowledge, production experience, and manufacturing resources supports the development of specialized tooling for different can-making applications.
Tooling design begins with understanding the application. Engineers need to consider the lid profile, material characteristics, press configuration, production requirements, and interface with other components. A design that works well on one press may not be suitable for another press if the stroke, mounting system, or forming sequence is different.
The company’s engineering approach is influenced by practical experience in can-making production. Its product design principles are similar to those associated with established international can-making machinery concepts, including systems connected with KRUPP, SOUDRONIC, and ALFONS-HAAR. At the same time, the company combines these design principles with experience gained from actual production environments and customer applications.
This practical approach is important because a mold is not an isolated component. It works as part of a mechanical system. Factors such as feeding accuracy, press alignment, clearance, lubrication, and operator adjustment can affect the final result. Engineers who understand the complete can-making process are better positioned to develop tooling that is suitable for real production conditions.
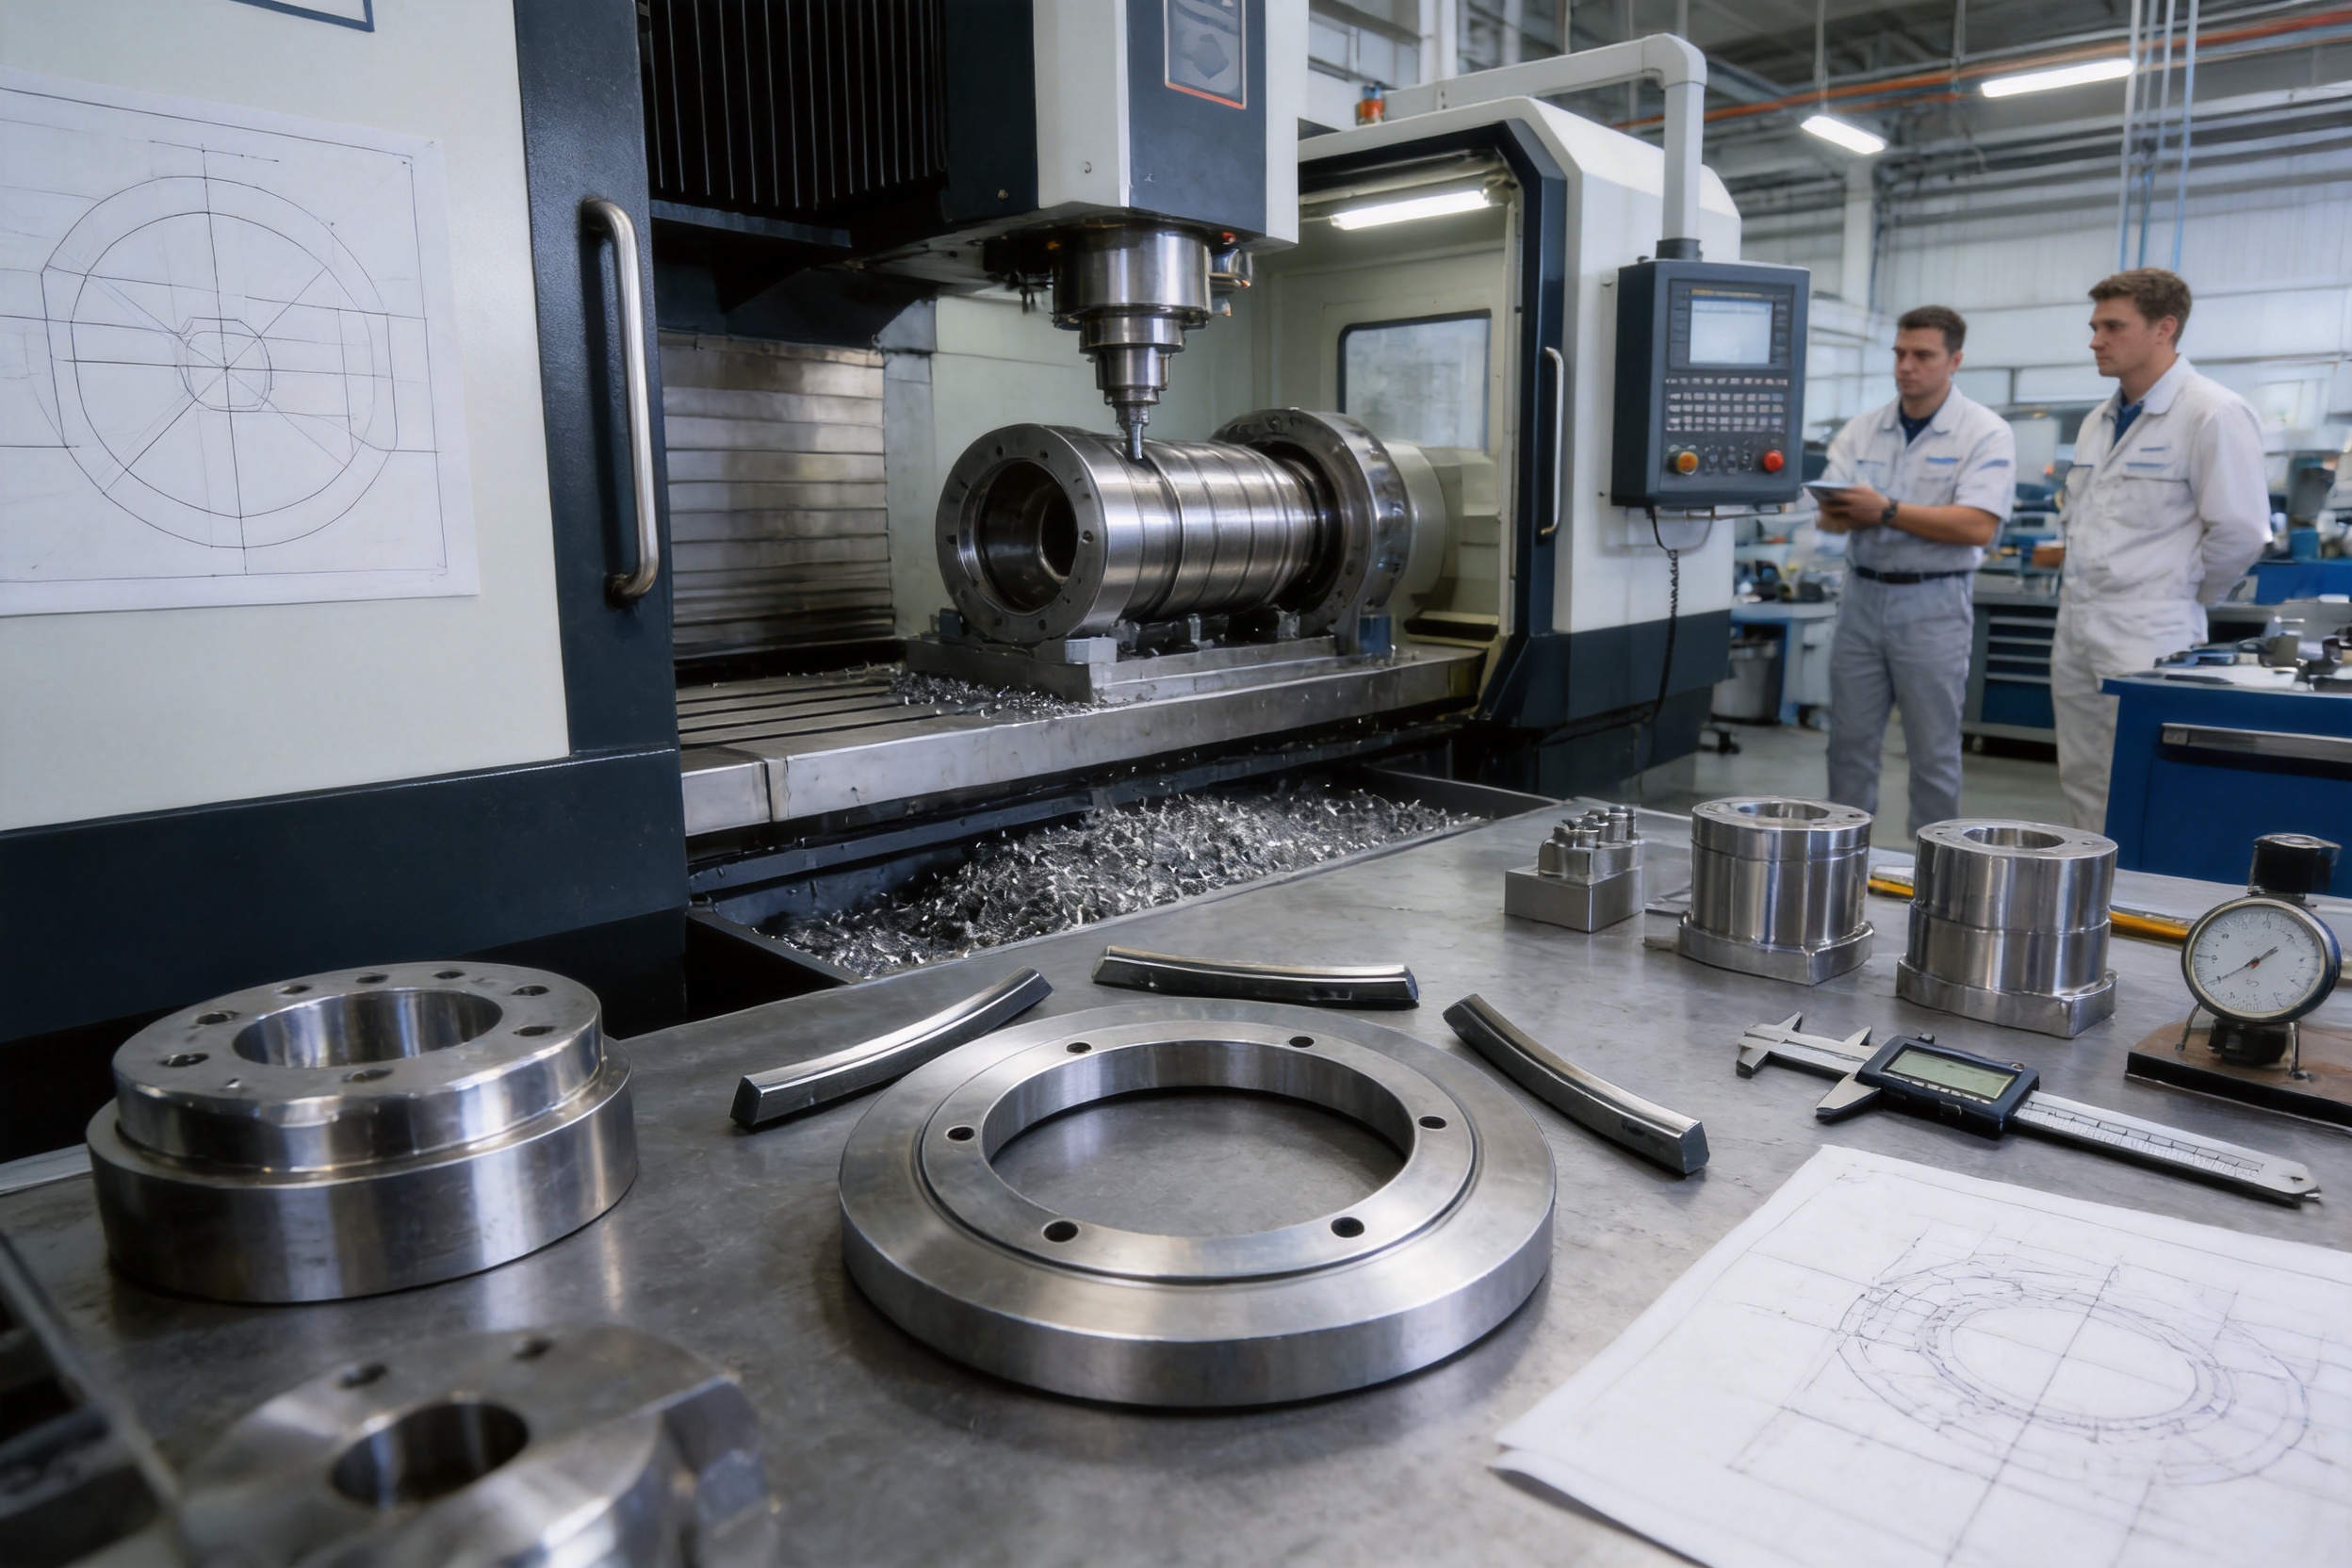
The company uses CNC high-precision machining equipment together with complete mechanical processing equipment. CNC machining supports repeatable production of complex profiles and helps maintain dimensional consistency from one component to another. It is particularly useful when a die contains carefully controlled radii, transitions, mounting features, or multiple related surfaces.
High-precision machining also supports replacement tooling. When a customer needs another die with the same profile, a controlled manufacturing process makes it easier to reproduce the original dimensions. This can be important for plants that operate several similar presses or maintain spare tooling for critical production lines.
Machining quality should be assessed across the complete process, not only by the final visible appearance. Important areas include material preparation, workholding, tool selection, cutting control, dimensional inspection, surface finishing, and protection during storage and shipment. Each stage contributes to the reliability of the final roller die.
In addition to CNC equipment, complete mechanical processing resources give the manufacturer greater control over supporting operations. These may include conventional machining, grinding, drilling, turning, finishing, fitting, assembly, and inspection activities, depending on the specific tool design.
Having multiple processes available within one manufacturing organization can improve coordination between departments. It may also help reduce delays caused by transferring precision components between unrelated suppliers. For customers, this can simplify communication because design, production, technical clarification, and after-sales support are handled through a coordinated source.
Zhejiang Golden Eagle Food Machinery Co., Ltd. has been certified to the ISO9001 quality management system and ISO14001 environmental management system. ISO9001 provides a structured framework for quality-related processes, documentation, control, and continual improvement. ISO14001 reflects attention to environmental management and the control of environmental responsibilities within manufacturing operations.
Certification does not replace product-specific inspection, but it demonstrates that the company has established formal management systems. For an industrial customer, this can provide additional confidence when evaluating a supplier for repeat orders, customized tooling, and complete production equipment.
The company has produced more than 10,000 pieces of can and can-lid equipment. Its product range includes machinery and molds for food cans, beverage cans, can lids, chemical tanks, aerosol canisters, two-piece cans, and pop cans. This breadth of experience is relevant to tooling customers because the performance of a roller die is closely connected with the wider production process.
A supplier that understands only one small tooling operation may not recognize how a die affects feeding, forming, seaming, inspection, and final packaging. A supplier with experience in complete lines can assess the tool in relation to the entire workflow. This broader perspective may help customers identify compatibility risks before manufacturing begins.
Price is often an important consideration when purchasing replacement tooling, but the purchase price does not represent the complete cost. A low-cost die may appear attractive until it causes higher rejection rates, frequent adjustments, premature wear, or repeated downtime.
| Evaluation Area | Precision Conversion Press Seaming Roller Die | Low-Quality or Poorly Matched Alternative |
|---|---|---|
| Dimensional accuracy | Designed and machined according to defined tooling data | May rely on approximate dimensions or inconsistent reproduction |
| Surface finish | Controlled working surfaces help reduce friction and marking | Rough areas or burrs may damage the metal surface |
| Press compatibility | Can be matched to the press, lid specification, and forming sequence | May require excessive adjustment or may not function correctly |
| Production stability | Supports repeatable forming during continuous operation | May produce variation as operating conditions change |
| Tool life | Supported by suitable manufacturing processes and maintenance planning | May wear quickly because of material or finishing limitations |
| Technical support | Can be supported by engineering and can-making experience | Support may be limited to basic dimensional supply |
| Total operating cost | Potentially lower through reduced waste and downtime | May create hidden costs through rejects and interruptions |
The comparison does not mean that every alternative supplier produces inferior tooling. It highlights the importance of evaluating the manufacturing process, technical documentation, inspection capability, and application support rather than comparing unit prices alone.
Food cans require dependable closure performance and consistent internal protection. Their lids may include countersunk areas, curls, beads, or other features designed for handling and seaming. A precision roller die helps produce the required geometry while minimizing avoidable damage to the coated metal surface.
Food can lines may operate at high volume, making stable tooling especially important. Even a small increase in rejected lids can create significant material loss over a long production run. Consistent forming therefore contributes to productivity, quality control, and cost management.
Beverage packaging commonly demands high-speed production and close dimensional control. Lids and ends must be fed reliably and presented accurately to downstream processes. The conversion press tooling must therefore be designed for the required production speed and metal specification.
Because beverage packaging lines may run continuously for extended periods, tool inspection, lubrication, alignment, and replacement planning are essential. A suitable seaming roller die supports the repeatability needed for automated handling and quality inspection.
Aerosol containers and components may require specialized shapes and carefully controlled forming transitions. Depending on the product design, tooling may be used for cones, domes, ends, or other formed components. The die profile must be matched to the material and the intended pressure and sealing requirements of the final container.
In these applications, surface quality and profile accuracy are important because the formed part may need to connect with additional components. A properly manufactured die helps reduce defects that could interfere with assembly or later testing.
Chemical containers often require robust construction and dependable closure systems. Their metal thickness, material type, and forming requirements may differ from those of food or beverage cans. Tooling should be developed around the actual tank or container specification rather than transferred without review from another application.
The manufacturer’s experience with chemical tank production lines provides a broader foundation for handling specialized metal packaging requirements. Technical review is still necessary for each individual product, particularly when the container will hold aggressive or regulated materials.
Two-piece cans use a different general manufacturing concept from traditional three-piece cans, but forming and end-making tooling remain critical to the final packaging system. The conversion press seaming roller die may be used where the lid or end requires a defined profile before attachment or closure.
Tooling selection should consider the relationship between the formed end and the can body, as well as the requirements of the subsequent seaming, testing, and filling processes.
Customers should provide sufficient technical information before ordering a conversion press seaming roller die. The more complete the information, the more accurately the supplier can confirm compatibility and prepare the tooling.
Useful press details include the machine manufacturer, model, working stroke, rated capacity, operating speed, mounting method, available space, and existing tooling arrangement. Drawings or photographs of the current installation may also help clarify the required interface.
The supplier should receive the relevant dimensions of the lid and can body. These may include outside diameter, inside diameter, curl dimensions, countersink dimensions, bead geometry, panel depth, score location, flange dimensions, and other features included in the product drawing.
It is important to distinguish between nominal dimensions and actual production measurements. If the customer is replacing an existing die, samples of acceptable and defective parts may help the engineering team understand the current production condition.
Material data should include the metal type, thickness, temper, coating, and any relevant mechanical properties. Different materials flow differently during forming. A tool profile that is suitable for one material may produce excessive stress or insufficient forming when used with another.
Customers should state the expected production speed, operating schedule, annual output, required service life, and quality standards. A die designed for occasional production may not be appropriate for a high-volume continuous line. Conversely, a heavy-duty configuration may be unnecessary for a low-volume application.
If the order is intended to solve a current production problem, customers should describe the symptoms clearly. Relevant information may include wrinkling, tearing, scratches, inconsistent curl, dimensional drift, material sticking, abnormal noise, excessive wear, or poor seaming results.
Providing this information helps distinguish between a tooling problem and other possible causes such as press misalignment, incorrect clearance, inadequate lubrication, worn bearings, unstable feeding, or incorrect adjustment.
A professional tooling process normally begins with technical confirmation. The customer’s drawings, samples, machine information, and production requirements are reviewed before the design is finalized. This stage is important because an accurate tool made to incorrect or incomplete data will not deliver the expected result.
After design confirmation, material preparation and machining are carried out according to the approved requirements. CNC high-precision machining can be used for the critical profile and related features. Supporting mechanical processes are applied where needed to create mounting surfaces, holes, shafts, transitions, and other components.
Finishing is performed to achieve the required surface condition. Working surfaces should be free from damaging burrs and unsuitable irregularities. The final finish depends on the material, forming function, and customer specification.
Inspection should verify critical dimensions, profile accuracy, surface condition, mounting features, and overall conformity with the approved drawing. Where applicable, the tool may be checked against reference gauges, coordinate measurement procedures, or assembly requirements.
Final fitting and trial evaluation may be included depending on the project. A trial run can help confirm that the die interacts correctly with the related punch, roller, guide, and press components. If the customer requests a complete machine or line, the tooling can be evaluated as part of the broader equipment system.
Correct installation is essential for obtaining the intended performance from a conversion press seaming roller die. Before installation, the operator should clean the mounting area and confirm that no chips, burrs, oil contamination, or foreign particles are present on the contact surfaces.
The die should be installed according to the approved machine drawing or supplier instructions. Fasteners, locating features, clearances, and alignment should be checked carefully. Excessive force should not be used to fit a component into position. If the die does not seat correctly, the cause should be investigated rather than corrected by unauthorized grinding or modification.
After installation, the press should be operated at a safe inspection speed where possible. Initial samples should be measured and visually inspected before the machine is returned to full production speed. Operators should check the formed profile, surface condition, dimensions, and interaction with downstream equipment.
Lubrication must follow the requirements of the press and the material being formed. Too little lubrication may increase friction and wear, while excessive or unsuitable lubrication may contaminate the product or affect the forming process. The correct lubrication method should be confirmed with the equipment and process team.
Operators should also monitor unusual noise, vibration, heat, material movement, and changes in product quality. Early detection of abnormal conditions may prevent damage to the die and related machine parts.
Routine maintenance is necessary even when the die is manufactured to a high standard. At suitable intervals, the working surfaces should be cleaned and inspected for scratches, built-up material, corrosion, wear patterns, and other changes.
Maintenance personnel should compare current production samples with the original approved dimensions. A gradual change in the lid profile may indicate normal tool wear, incorrect adjustment, press alignment issues, or wear in an associated component. Monitoring trends is more effective than waiting for a complete failure.
When cleaning the die, tools and chemicals that may scratch or attack the working surface should be avoided. After cleaning, the component should be dried and protected according to the storage requirements. If the die will not be used for an extended period, appropriate corrosion protection and packaging should be applied.
Replacement timing should be based on measured performance rather than a fixed assumption alone. Factors to consider include rejection rate, dimensional variation, surface marks, forming force, inspection results, and the tool’s operating history. Maintaining a spare die can also reduce downtime during planned maintenance or unexpected repair.
A conversion press seaming roller die is closely related to the rest of the can-making system. Choosing a supplier with experience in both molds and machinery can offer several practical advantages.
First, the supplier is more likely to understand how the die interacts with the press and associated tooling. This may improve the accuracy of technical communication and reduce the risk of supplying a component that fits physically but performs poorly in operation.
Second, an experienced supplier can support broader production requirements. Customers may need not only a replacement die but also automatic feeding machines, tin can lid end-making machines, cutting machines, welding machines, aerosol can equipment, two-piece can equipment, or a complete production line. A supplier with a broad product portfolio can help coordinate tooling and machinery requirements.
Third, after-sales support becomes more meaningful when the supplier understands the complete process. Zhejiang Golden Eagle Food Machinery Co., Ltd. provides installation, commissioning, technical guidance, operation training, and parts supply. These services can help customers place new equipment into operation and maintain production after delivery.
Finally, a long-established manufacturer is able to draw on accumulated application knowledge. Since its establishment in 1978, the company has supplied equipment and molds to customers in Europe, Asia, Africa, North America, South America, and Oceania. International project experience may help the company work with different production standards, machine configurations, communication requirements, and customer expectations.
For a can manufacturer, the value of a conversion press seaming roller die can be considered in several practical areas:
Production continuity: Stable tooling helps reduce interruptions caused by premature wear, poor fit, or inconsistent forming.
Product quality: Controlled profiles support more uniform lids and improved compatibility with downstream seaming and inspection equipment.
Material utilization: Fewer defective parts can reduce scrap and improve the use of tinplate or other metal materials.
Maintenance planning: A durable and traceable die makes it easier to schedule inspections, spare-tool preparation, and planned replacement.
Line integration: Tooling designed with the press and production process in mind can support more reliable automatic operation.
Technical confidence: Engineering support and after-sales service help customers address installation, commissioning, and operating questions.
Long-term cooperation: A supplier capable of producing both machinery and molds can continue supporting future product changes, capacity expansion, and replacement requirements.
It is a precision tooling component used to form a specified profile on a metal can lid or end during a conversion press operation. The formed profile supports later handling, assembly, and seaming of the container.
No. Compatibility depends on the press model, mounting arrangement, forming sequence, lid dimensions, material, and operating conditions. Technical information should be confirmed before manufacturing or ordering a replacement.
Custom tooling can generally be developed according to customer drawings, samples, press data, and product requirements. The final design should be confirmed by the manufacturer’s engineering team before production.
Useful information includes the press model, existing tooling drawing, lid or end drawing, material type, material thickness, production speed, required quantity, photographs of the installation, and a description of any current production problems.
It helps maintain the intended forming profile, reduce dimensional variation, limit surface damage, improve repeatability, and support reliable interaction with downstream seaming equipment. The actual result also depends on machine condition, adjustment, lubrication, material quality, and operator practice.
Service life varies according to material, production speed, pressure, lubrication, alignment, maintenance, and the geometry of the product. A realistic service-life estimate should be discussed with the supplier using the customer’s operating conditions.
The die should be kept clean, inspected at regular intervals, protected from corrosion, and checked for wear or surface damage. Operators should monitor changes in product dimensions and forming quality and should not make unauthorized modifications to the working profile.
Zhejiang Golden Eagle Food Machinery Co., Ltd. provides after-sales services including installation, commissioning, technical guidance, operation training, and parts supply. The specific support available should be confirmed for each order and project.
No. Conversion press tooling may be used in various metal packaging applications, including food cans, beverage cans, aerosol containers, chemical tanks, and other can or lid production systems. The die must be designed for the specific application.
A controlled surface finish helps reduce friction, material marking, built-up residue, and premature wear. It also supports smoother movement of coated metal through the forming operation.
The company supplies complete series of can-making machinery and molds, including food can, beverage can, can lid, chemical tank, aerosol canister, two-piece can, and pop can production equipment. Customers can discuss whether the tooling should be integrated into a larger project.
The conversion press seaming roller die is a small but highly influential component in metal can and lid manufacturing. Its dimensional accuracy, surface finish, durability, and compatibility with the press directly affect forming stability and downstream seaming performance. For high-volume manufacturers, selecting a precision-engineered die can contribute to lower scrap, fewer adjustments, reduced downtime, and more consistent product quality.
Zhejiang Golden Eagle Food Machinery Co., Ltd. combines long-term can-making experience with engineering resources, CNC high-precision machining equipment, complete mechanical processing capability, quality management certifications, and after-sales technical support. Its experience in producing can-making machines and molds allows the conversion press seaming roller die to be considered as part of a complete production system rather than as an isolated replacement component.
Customers evaluating this type of tooling should provide accurate press and product information, confirm the forming requirements, review inspection criteria, and establish suitable maintenance procedures. With proper technical matching and professional manufacturing, the die can provide a dependable foundation for efficient and repeatable tinplate can lid production.
1. General principles of metal forming and sheet-metal press tooling.
2. Industrial practices for tinplate can manufacturing, lid forming, and double-seam preparation.
3. Quality management principles for precision mechanical manufacturing.
4. Environmental management principles for industrial equipment and tooling production.
5. Technical information supplied for Zhejiang Golden Eagle Food Machinery Co., Ltd. and its can-making machinery and mold manufacturing operations.
6. General maintenance practices for conversion presses, forming dies, rollers, and can-making production lines.
Related Products
Founded in 1978, the company is one of the largest can-making machinery well-known companies at home and abroad.
Product Categories
Contact Information
Zhongshatou Shenjiamen Zhoushan Zhejiang China
+86-580-3056646
 English
 中文简体
 русский
 عربى
 Español