2026-10-15
A production manager orders a tinplate can making machine expecting to run 500 cans per minute. The welder arrives, passes its factory test, and then sits idle for two weeks because the seamer cannot match its speed, the slitter produces burrs, and the tooling for a planned 2026 can size was never quoted. The machine itself is rarely the bottleneck. The line balance, tooling package, and material tolerance usually decide whether a tinplate can making machine pays for itself in one year or three.
This article explains what a tinplate can making machine actually includes, how the core process flows from coil to finished can, and which selection criteria matter most for food, beverage, aerosol, and chemical can production.
A tinplate can making machine is not a single unit. It is a coordinated set of equipment that turns tin-coated steel coil into a printed, welded, coated, and seamed can. For three-piece cans, the line usually includes a decoiler, a duplex slitter, a body welder, a side-seam coating and drying unit, a combiner or flanger, a seamer, and inspection stations. For two-piece cans, the process changes to cup forming, drawing, wall ironing, trimming, and necking, but the same principle applies: every station must pass cans at a compatible rate.
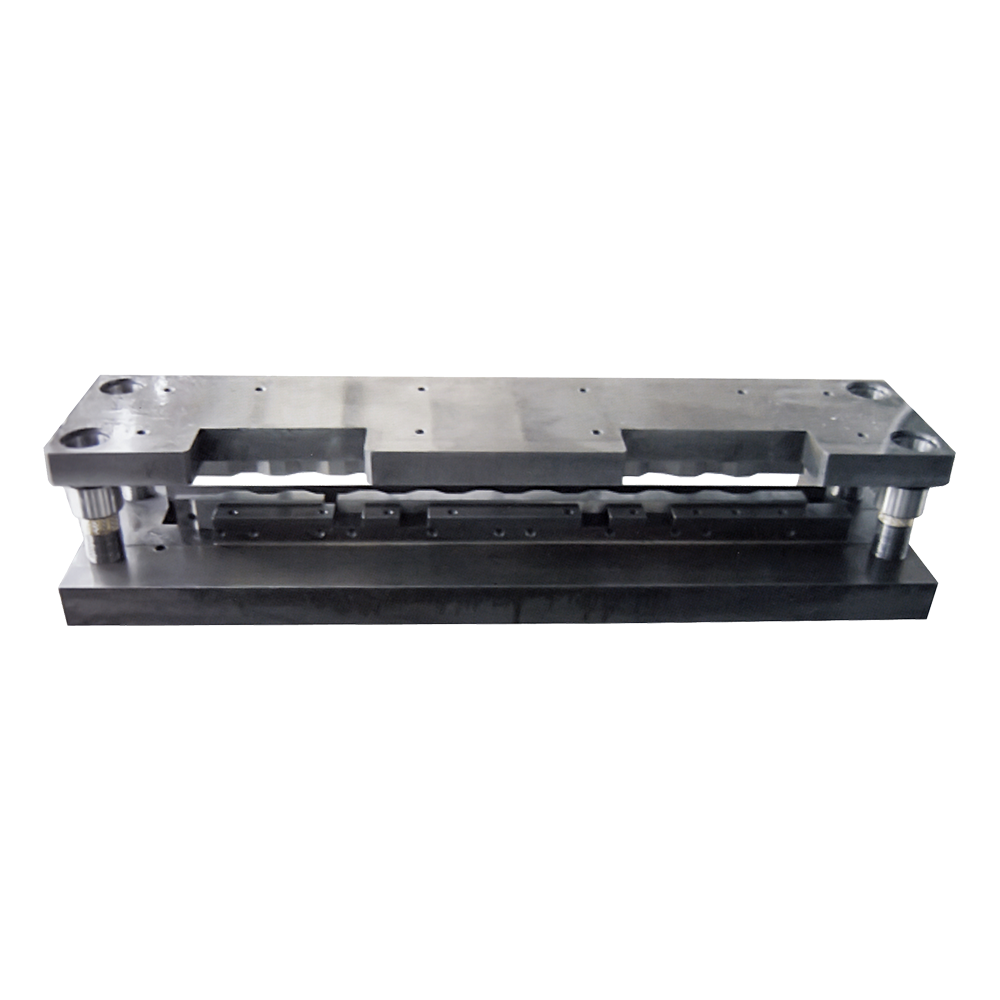
The term also covers tooling and molds. A conversion press channel die, a CNC pressing die, or a seaming roller determines whether the finished can meets dimensional tolerance. Buyers who treat tooling as an accessory often discover that spare molds cost more than the original budgeted amount.
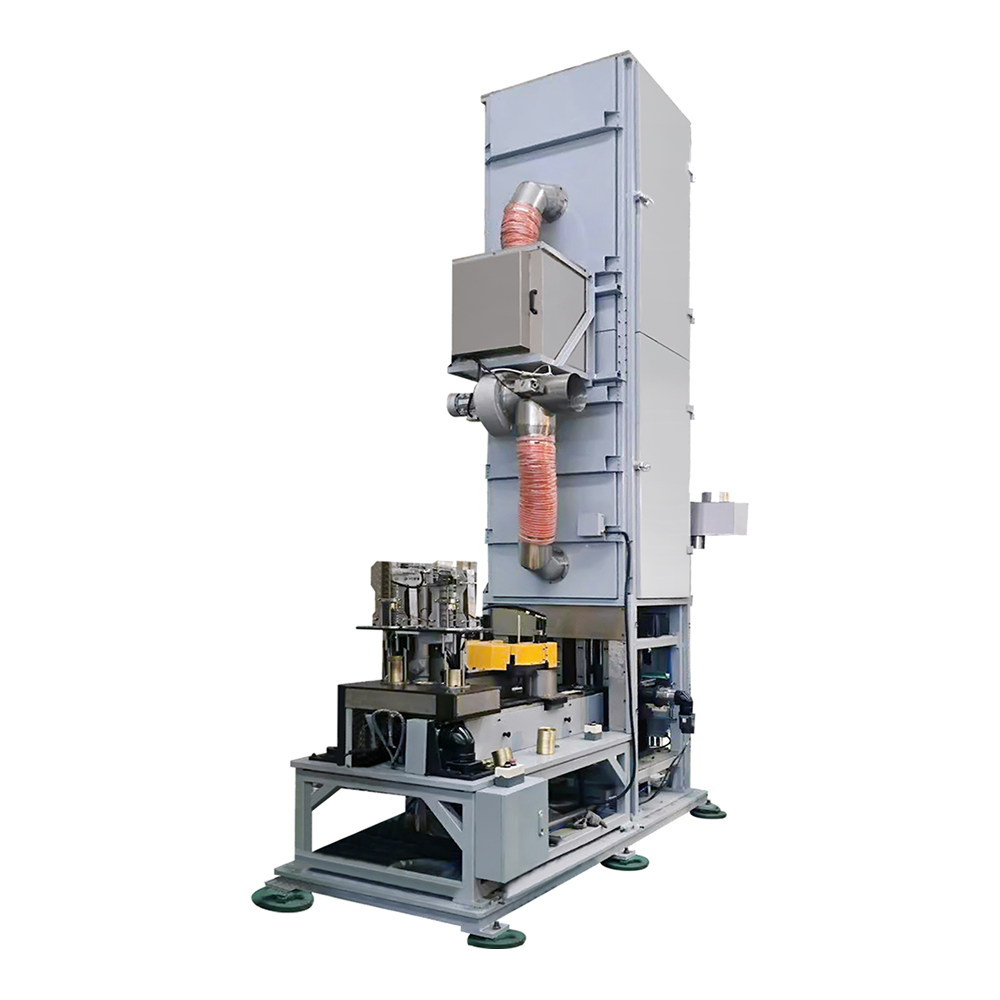
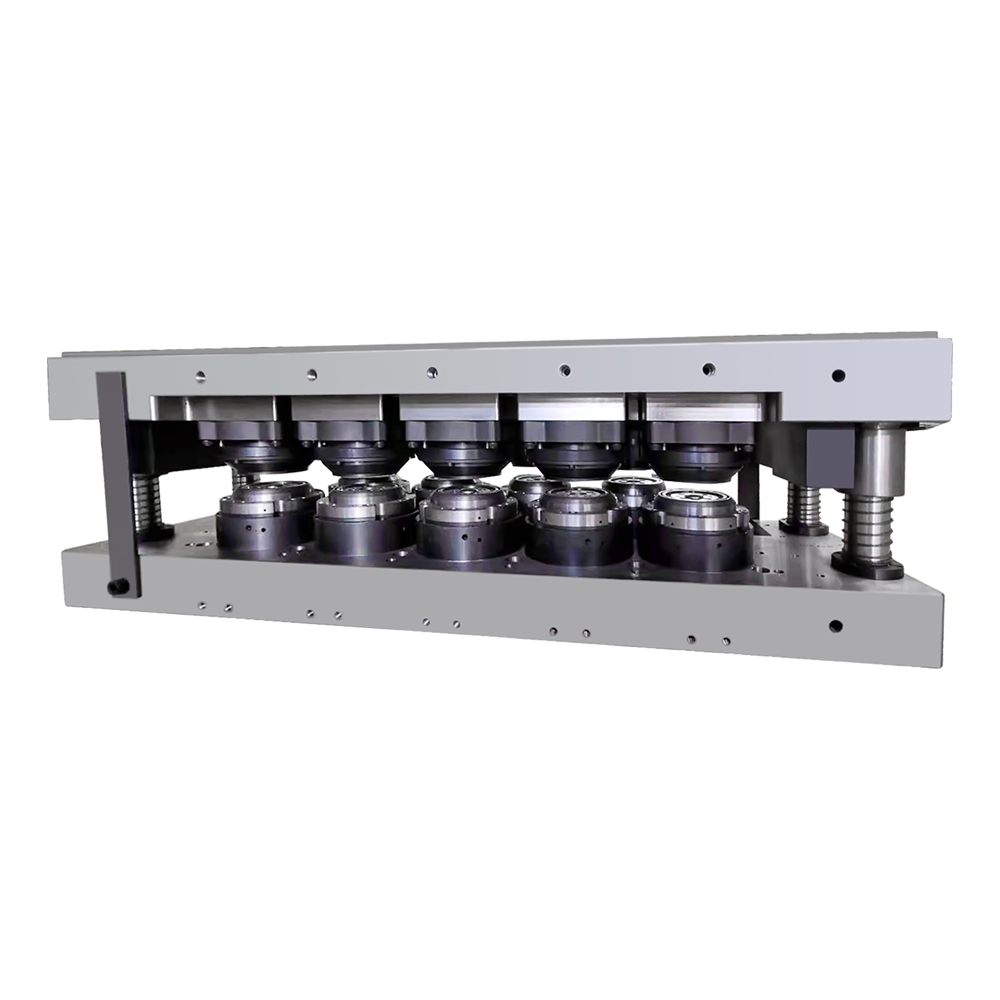
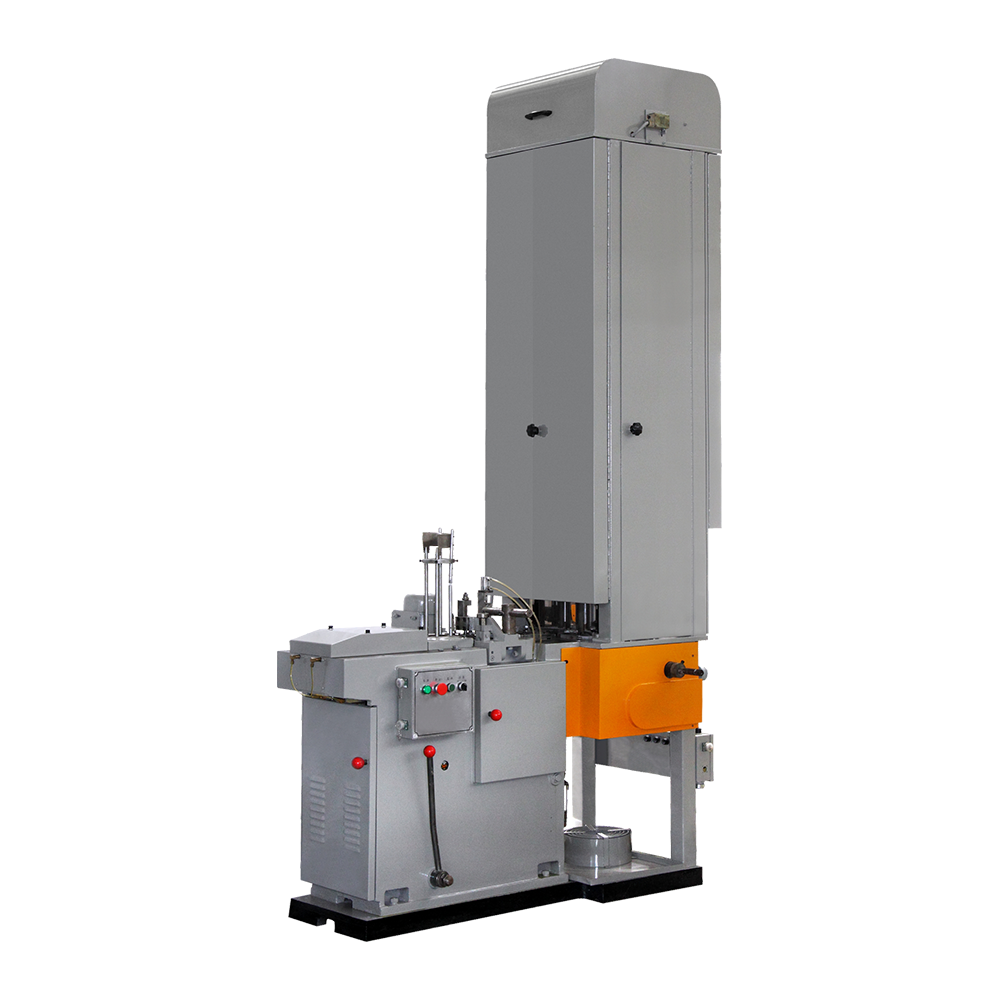
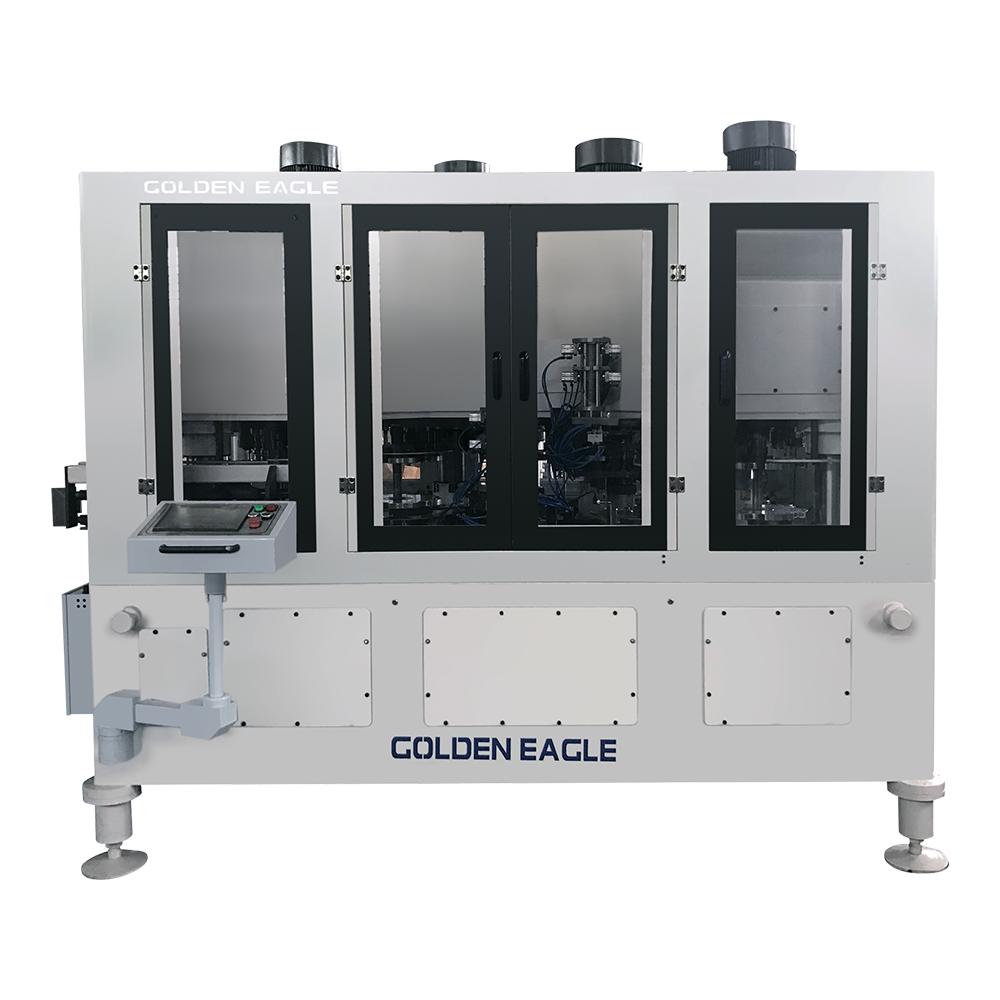 Four-Station Can Making Machine for Necking Flanging Beading SeamingProduct page lists GT3B series models for food and beverage can production, covering necking, flanging, beading, and seaming with OEM/ODM options.View Product →
The sequence below is typical for a three-piece tinplate can line. Speed ranges are general industry references, not guarantees, because actual output depends on can diameter, material thickness, and the weakest station in the line.
The first practical step is slitting. A duplex slitter cuts wide tinplate coil into body blanks of the required width. Burrs or camber here cause welding defects downstream. The body welder then joins the blank into a cylinder. For food cans, the welded seam receives a side-seam coating and drying pass to protect the exposed iron from corrosion. After that, the can body moves to a combiner or flanger, where the ends are prepared for seaming. The seamer rolls the end onto the body to form an airtight joint.
Two-piece beverage cans skip the welding step. Instead, a cupping press forms a shallow cup, and a body maker stretches the cup into a seamless can. This route suits high-volume beverage production, but it requires different tooling and a larger capital budget.
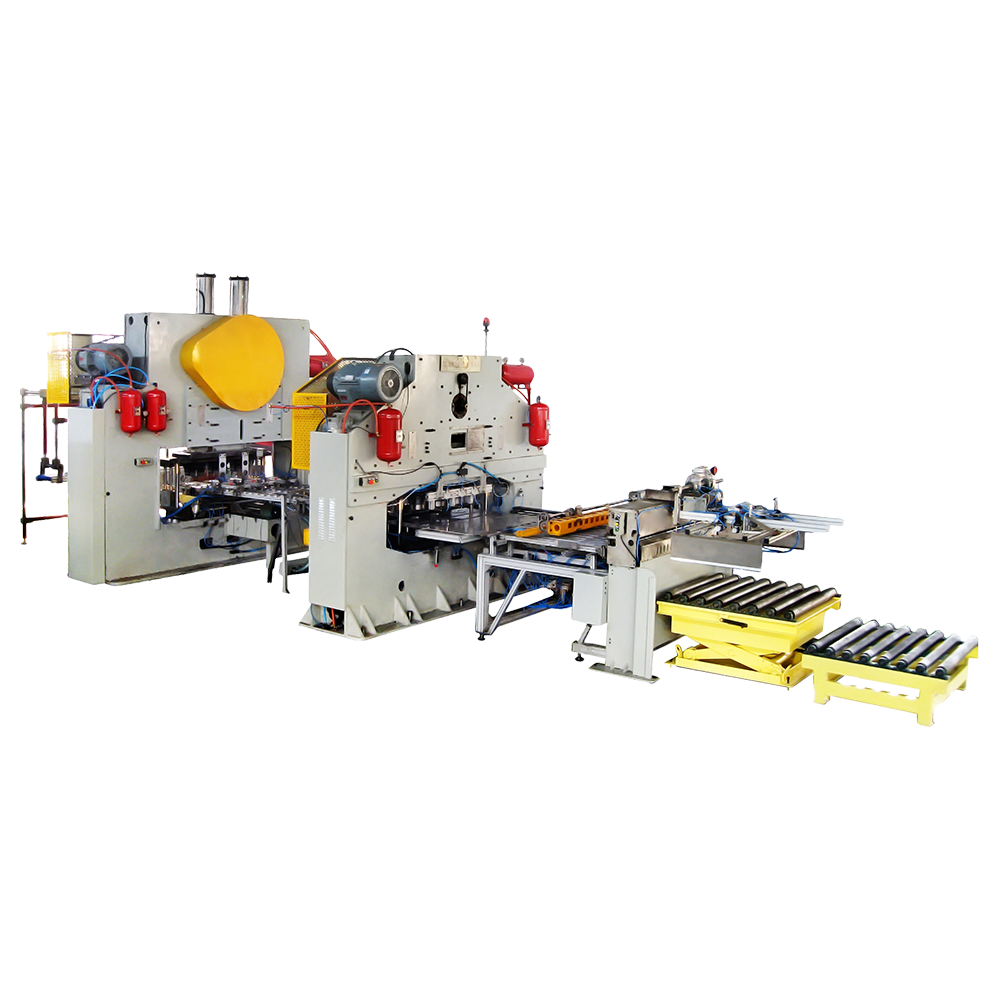
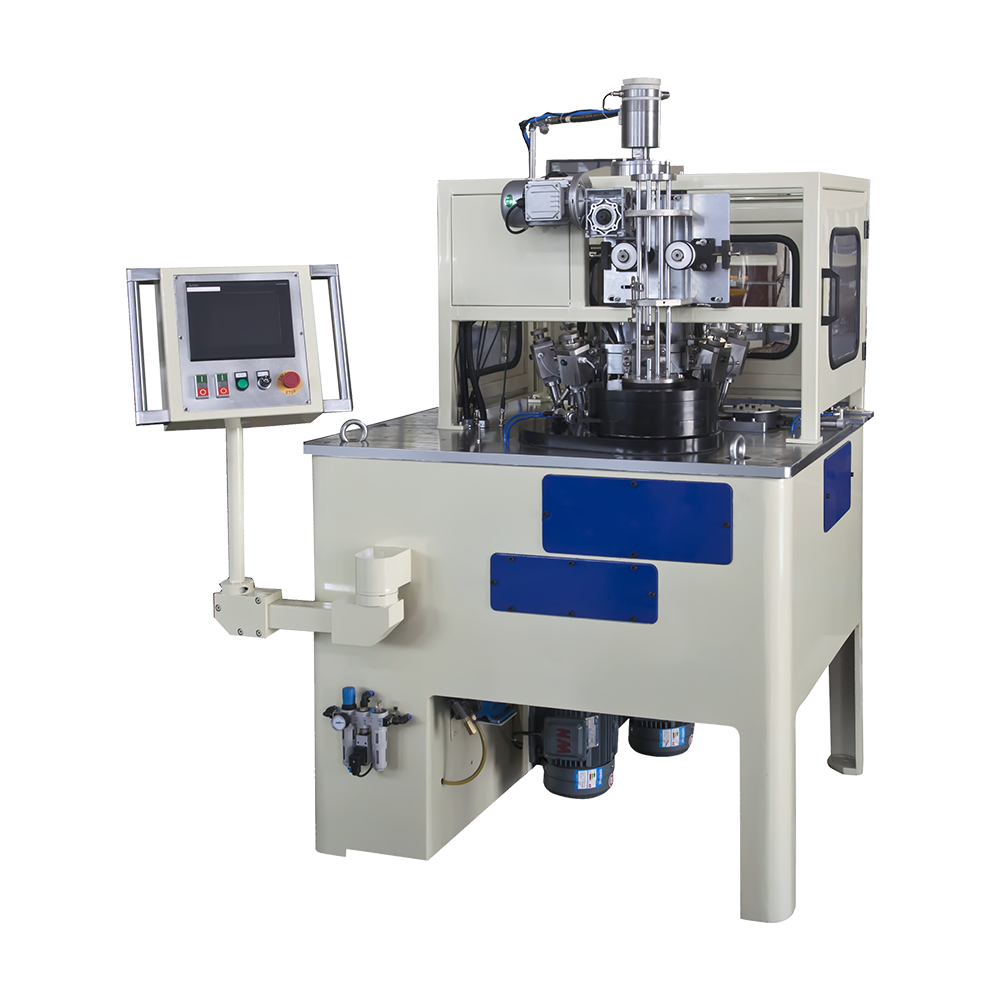
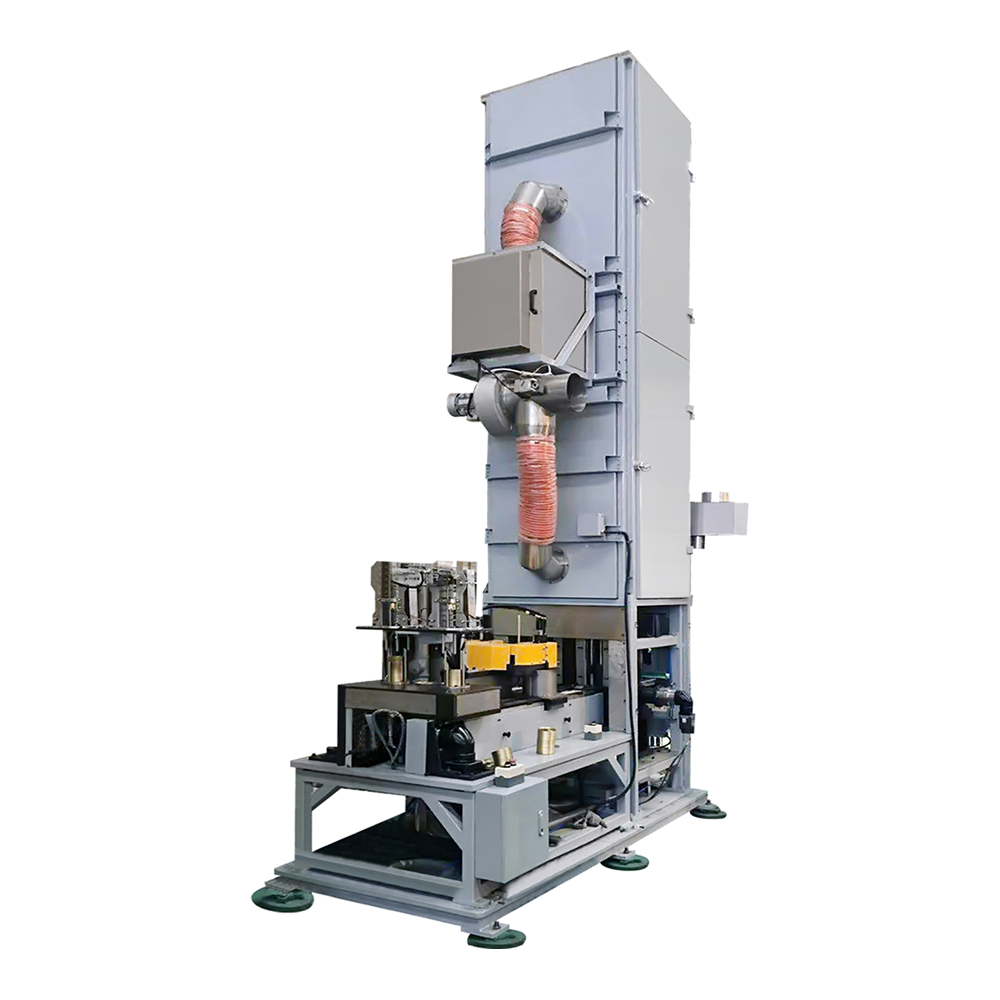
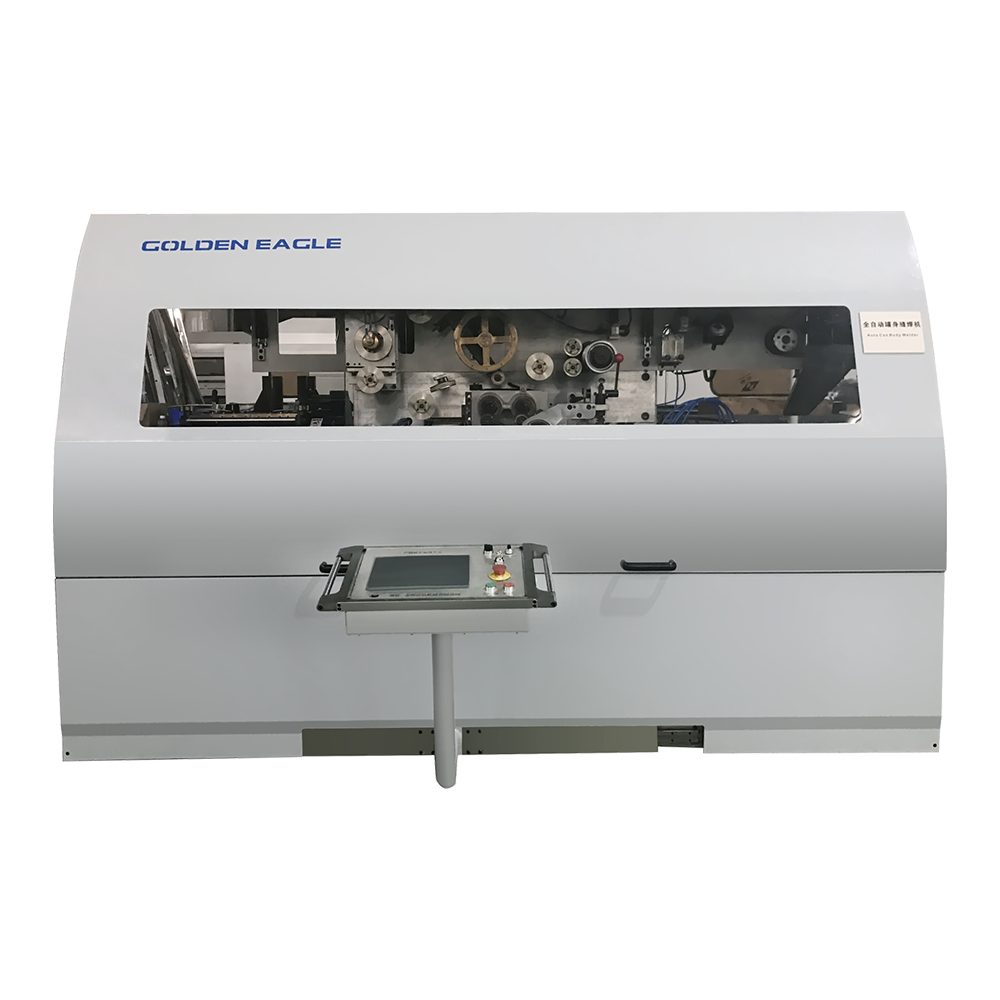 GT10C-500 Automatic High-Speed Can Body Seam WelderFor tin can body production, this automatic seam welder is listed at 500 cpm with can size ranges for food, beverage, and aerosol applications.View Product →
Start with the can, not the machine. A line specified for a 2026 can size may not handle a 2028 promotional shape without new tooling. The following criteria prevent most costly mismatches.
For a deeper checklist, see this guide on how to choose the right can making machine.
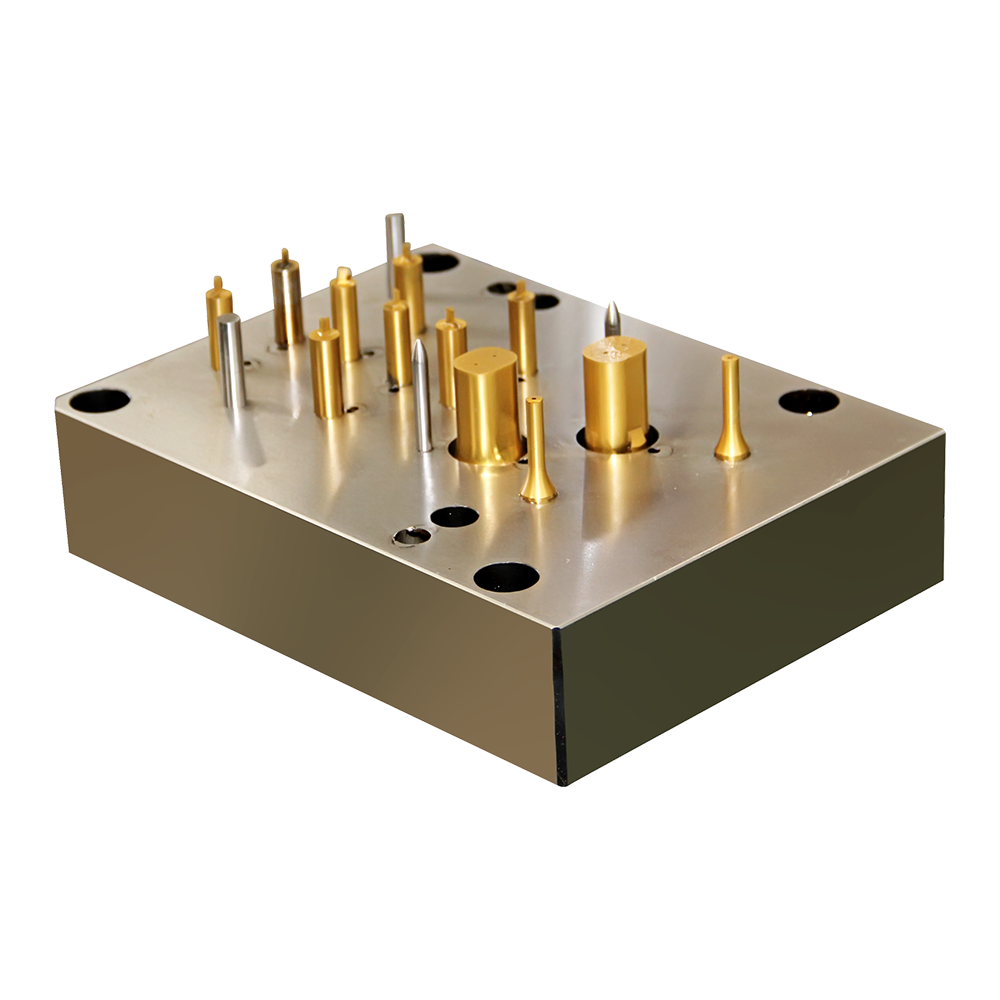
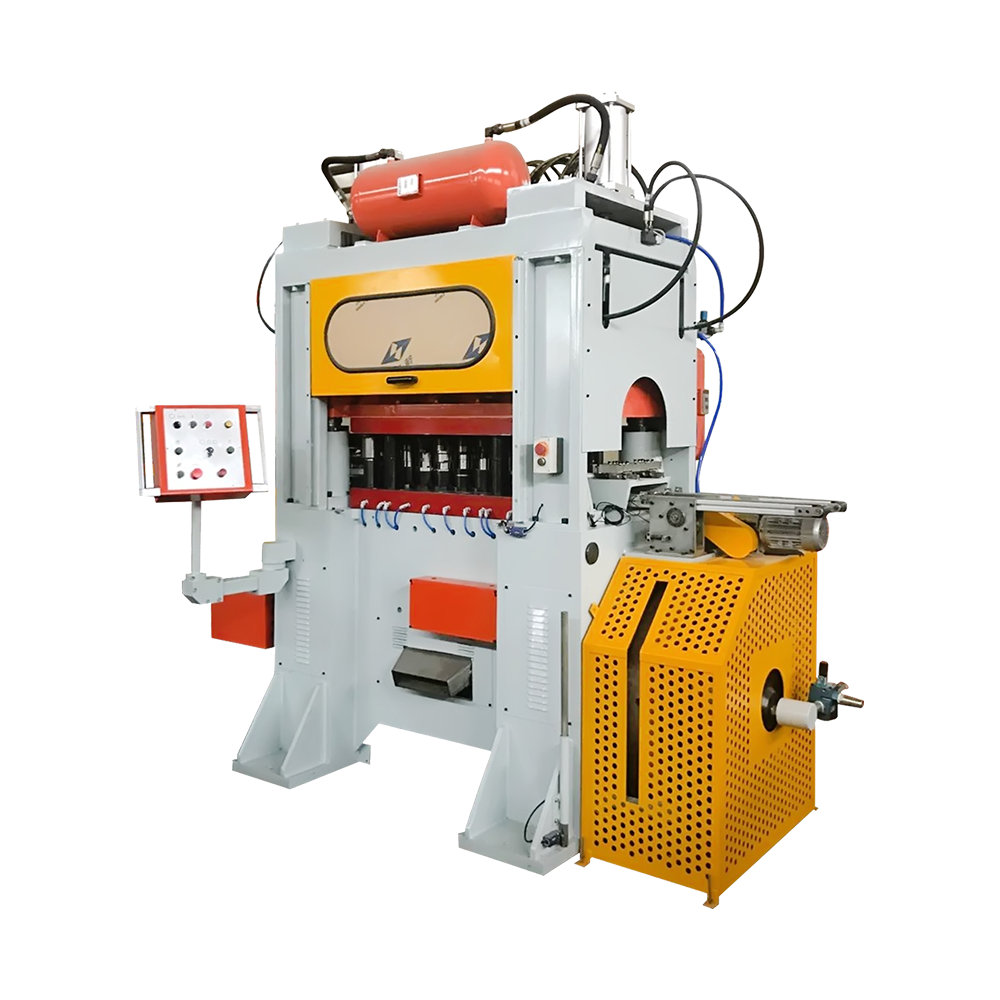
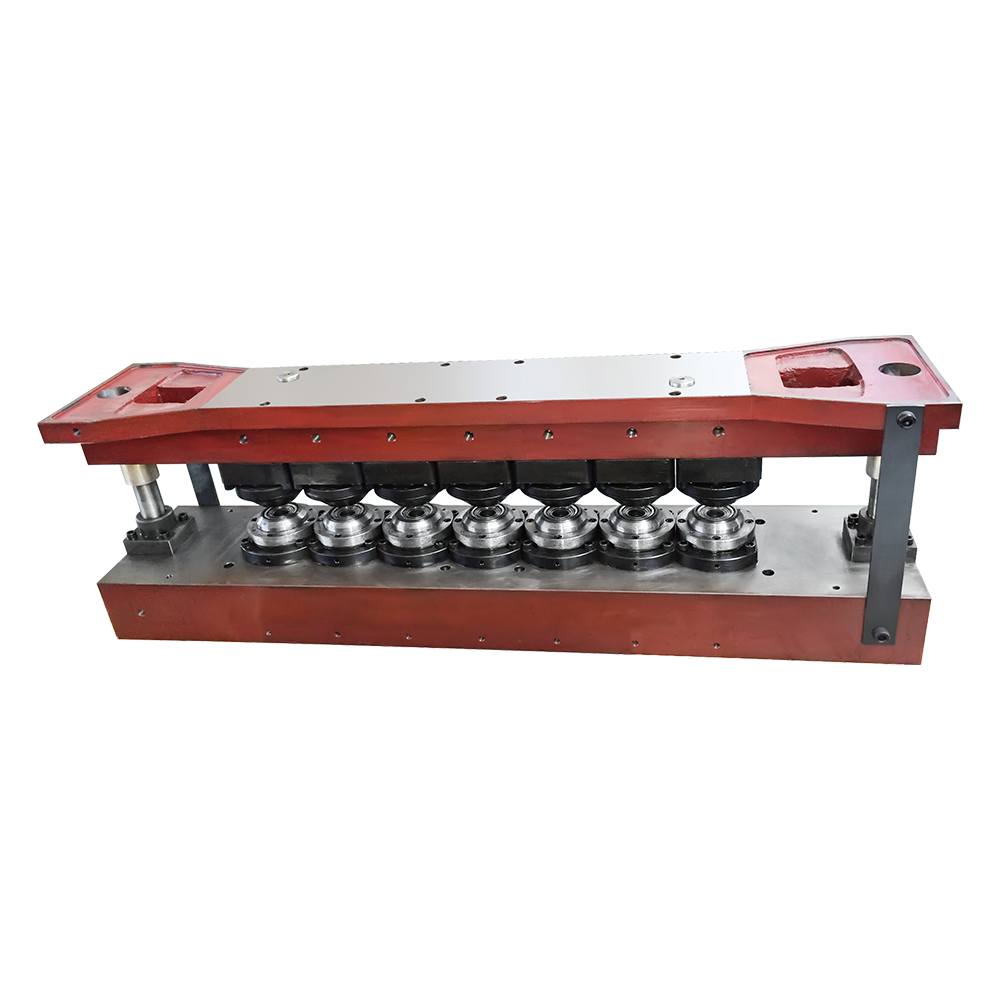 Conversion Press CNC Pressing Die for Can Making ToolingListed as a mold item with OEM/ODM availability, this CNC pressing die sits alongside conversion press seaming roller and channel die tooling.View Product →
Tinplate can making machines serve several can families. The table below compares the main routes and the equipment that changes between them.
| Can type | Typical material | Key equipment | Common industries |
|---|---|---|---|
| Three-piece can | Tinplate, ECCS | Duplex slitter, body welder, side-seam coater, combiner, seamer | Food, chemical, aerosol |
| Two-piece can | Aluminum, tinplate | Cupping press, body maker, trimmer, necking machine | Beverage, beer, soft drinks |
| Aerosol can | Tinplate | Cone/dome press, top cover punch, seamer, leak tester | Personal care, household, industrial |
| Milk powder can | Tinplate | Single or two-station combiner, seamer, lining machine | Dairy, infant formula |
Aerosol cans add a pressure requirement. The cone and dome must be formed to exact dimensions, and the seamer must create a leak-tight joint. For milk powder cans, the internal lining and compound application affect shelf life. If your product mix includes more than one can type, ask the supplier whether the same line can switch between them or whether a dedicated line is more economical.
Two identical tinplate can making machines can have very different uptime. The difference usually comes from maintenance discipline, operator training, and how spare parts are stocked. Reactive maintenance feels cheaper until a seaming roller fails during a peak order.
The figures above are illustrative ranges based on common industry experience. The exact numbers depend on line speed, shifts, and material. Still, the pattern holds: planned inspection of welding electrodes, seaming rollers, and cutting blades reduces unplanned stops. A simple daily check of lubricant levels and air pressure can prevent a full shift of lost output.
Operator training matters just as much. A welder set 5 percent too high may produce spatter, while a seamer with incorrect roll pressure creates leakers. Suppliers that offer on-site training and video documentation shorten the learning curve.
Before signing a purchase order, ask for a factory acceptance test using your actual tinplate material and can dimensions. A machine that passes with the supplier's sample may behave differently with your coil. Confirm the scope of supply: Does the price include tooling, installation, commissioning, and training? Are spare parts listed with lead times?
Also review the electrical and safety standards for your region. A machine built for one voltage or guarding standard may require modification before it can operate legally. Finally, request a list of reference installations running similar can types. A short call with an existing user can reveal more than a brochure.
A tinplate can making machine is a long-term asset. The best choice is not always the fastest or least expensive. It is the line that matches your can portfolio, your material, and your maintenance capability, with a supplier who can support it for the next decade.
Related Products
Founded in 1978, the company is one of the largest can-making machinery well-known companies at home and abroad.
Product Categories
Contact Information
Zhongshatou Shenjiamen Zhoushan Zhejiang China
+86-580-3056646
 English
 中文简体
 русский
 عربى
 Español